TEST
PROCESS
QUALIFICATION
ISO 9606-1 Welder Qualification Test: What Happens During the Certification Process?
By First Welding Certification Technical Editorial Team
8 Min Read
22Aug 2026
Table Of Contents
- Why Is the Qualification Test Needed?
- How Does the ISO 9606-1 Certification Procedure Take Place?
- What Is Checked in the Practical Welding Test?
- From a Test Piece to a Qualified Welder
- How Is the Test Piece Checked?
- What Is Done After Testing?
- Industrial Real-world Example: Steel Fabrication Company
- ISO 9606-1 Technical References
- Frequently Asked Questions
- Conclusion
- Ready for ISO 9606-1 Welder Qualification?
Key Takeaways
Define the welding conditions before testing
Demonstrate practical welding performance
Examine the completed test piece
Establish the applicable qualification range

Your welder might have lots of hands-on experience, but does that mean they’re ready for the specific welding job they’re about to do?
This is a question that comes up often for manufacturers, welding contractors, and quality managers.
Just because a welder is skilled in one type of welding process, position, or material doesn’t automatically mean they’re qualified for the process they’re about to use.Without a proper welding qualification test, it’s hard to know if their work meets the needed standards.
The ISO 9606-1 welder qualification test helps with that.
It lets you assess a welder’s skills by having them make a test weld under certain conditions, and then checking the finished weld against specific acceptance rules.
ISO 9606-1:2012 sets the rules for testing welders who do fusion welding on steel.
The standard focuses on checking if welders can control the welding process themselves and create a weld that’s up to standard.It applies only to manual and semi-automated welding methods, and doesn’t cover fully automated or mechanized welding.
For manufacturers, welding contractors, quality managers, and welding coordinators, knowing about the ISO 9606-1 certification process helps them understand the whole process—from preparing the test to the actual welding and checking the results.
Why Is the Qualification Test Needed?
A welder’s qualification isn’t just about knowing welding facts.It’s about showing real welding skills in specific situations.These situations include things like:
– How the welding is done
– What product is being welded
– The type of weld
– The base metal used
– The filler metal
– The size of the test pieces
– The position of the weld
– The welding standards followed
This is important because passing the test shows what kinds of welds the welder is qualified to do.
According to ISO, the ISO 9606-1 standard describes a test that makes sure welder qualifications are recognized the same way no matter where the welding is done, who does the testing, or what product is involved.
How Does the ISO 9606-1 Certification Procedure Take Place?
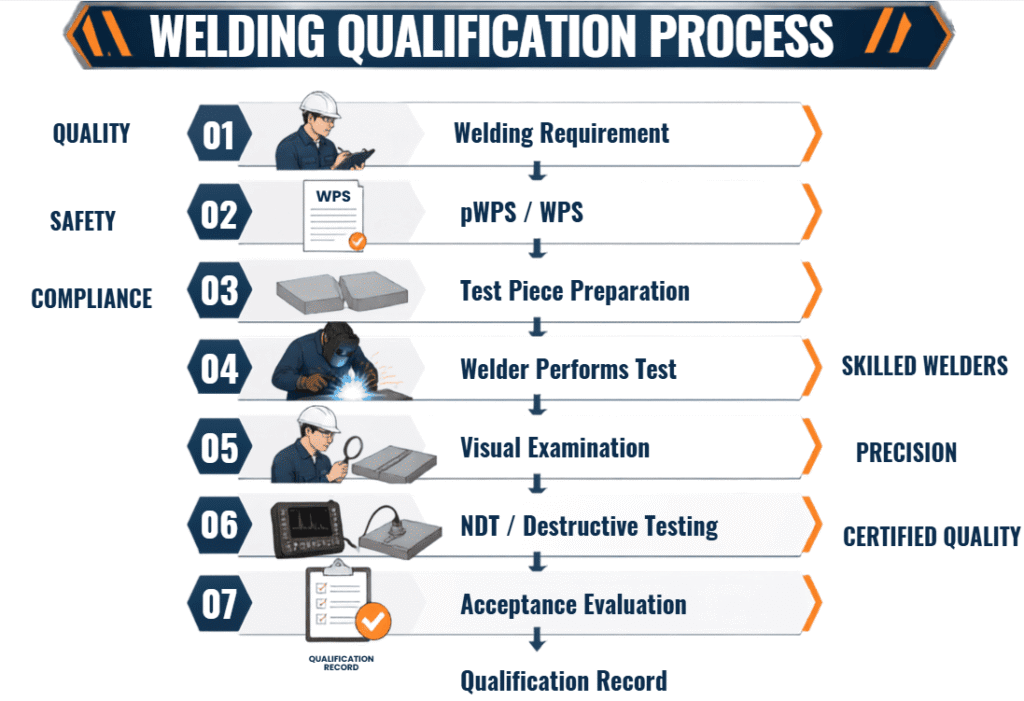
1.Requirement & Preparation — Figure out what needs to be welded, including the welding procedure specifications and the test conditions.
2.Test Piece & Welding — Set up the test piece and do the actual welding.
3.Examination & Evaluation — Check the weld with visual inspection, non-destructive testing, or destructive testing, and look at the results.
4.Qualification Record — Write down the successful outcome and decide the range of what this qualification covers.
1.Specify the Production Requirement
Before deciding on the qualifying test, it’s important to know what the weld is meant to do.
For example, a manufacturer might need a welder who can do things like:
– Weld steel plates
– Weld pipes
– Do butt welds
– Do fillet welds
– Work in a specific welding position
– Work on a certain type of material and thickness
The test needs to be set up with these production requirements in mind.
2.Determine the Welding Conditions
The right welding method and conditions are decided before the practical test.
These conditions must be clear because the qualification is connected to the settings used during the test.
3.Prepare the Test Piece
The test piece is chosen and set up according to the qualification needs.
Depending on what is needed for production, the test piece could be:
– A butt weld on plates
– A fillet weld on plates
– A butt weld on pipes
– A fillet weld on pipes
The material, size, how the joints are prepared, and other important test details are all recorded.
This helps to connect the actual test piece back to the qualification process.
What Is Checked in the Practical Welding Test?
The welder does the test weld by himself based on the test conditions, and the examiner watches the process.
The practical exam is very important under ISO 9606-1 because this standard highlights how important it is for the welder to have good control over the welding equipment manually.
The test piece is labeled so that the weld can be connected to the welder and the welding conditions.
Traceability during the Test
A well-done qualifying test creates a clear link:
Welder → Test Piece → Welding Conditions → Examination → Result
This traceability is especially important for manufacturers who keep records of their welders’ qualifications.
The role of the examiner or examining body is also very important in this process.
From a Test Piece to a Qualified Welder
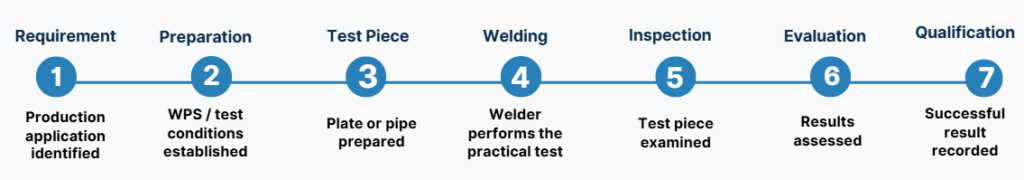
This is a timeline showing the steps in a process, not a set number of days. ISO 9606-1 gives the technical standards for qualification testing, but it doesn’t set a single time limit for each testing activity.
How Is the Test Piece Checked?
After the test piece is made, it is checked using a specific setup called the test configuration.
These setups might use different ways to check the test piece, such as:
– Visual testing (VT)
– Radiography (RT)
– Bend test
– Fracture test
– Macro test
The choice of these methods depends on the type of test piece and what is needed.
All these details are explained in Clause 6 of ISO 9606-1, which covers how testing and checking should be done.Clause 7 of the same standard talks about what standards the test piece must meet to be accepted.
For example, a butt weld test might involve visual inspection and other tests that are required for that specific test piece.
The main goal of this process is to see if the weld meets the required acceptance standards, not just to check if it passes a visual inspection.
What Is Done After Testing?
When a welder passes the exams, their qualification details will be officially recorded.
Clause 10 of ISO 9606-1 says that after passing the welder’s qualification test, the essential variables must be checked and recorded.
If a test is failed, no certificate will be given for that failure.The certificate is issued by the examiner or the examining organization.
Retests can also be done according to the standard.
This means that the outcome is based on both the test and the examination process, not just on performing the welding.
In the second part, which focuses on understanding the information in the document, read:
ISO 9606-1 Welder Qualification Certificate: A Field-by-Field Guide
For details on validity, continuity, and renewal, read:
ISO 9606-1 Welder Qualification: Validity, Continuity & Renewal Explained (2026)
Industrial Real-world Example: Steel Fabrication Company
Let’s look at an example of a steel fabrication company that makes welded joints for an industrial use.
The production team decides on the welding method, the materials, the type of joint, the thickness, and where the weld will be made.
They then choose the right welding test and prepare the test sample.
The welder does the test weld under the specified conditions, and the testing or inspection company is there to watch the process.
After the test, the sample is checked using the right methods.
If it meets the required standards, the qualification details are recorded, and the range of what the welder is qualified to do is decided.
Before starting the actual welding work, the company checks the real production conditions against the welder’s qualification range.
This creates a clear connection between:
Production Needs → Proven Ability → Test Results → Qualified Work Range
For manufacturers, this kind of tracking is very helpful, especially when the welders’ records are part of the technical documents.
ISO 9606-1 Technical References
For those who want to see the technical reasons, here are the key points:
| ISO 9606-1 Reference | Main Subject |
|---|---|
| Clause 5 | Essential variables and qualification range |
| Clause 6 | Examination and testing |
| Clause 7 | Acceptance requirements |
| Clause 8 | Re-tests |
| Clause 10 | Welder's qualification test certificate |
ISO has now released ISO 9606-1:2012 as the latest version.This standard was most recently updated and confirmed in 2023, but ISO says it will soon be replaced by ISO/DIS 9606.
For people working with pressure equipment, there is a direct connection between the rules and this standard.
According to PED 2014/68/EU, Annex I, point 3.1.2, the joining of parts of pressure equipment that help keep pressure in place must be done by trained workers following proper methods.If the equipment falls into Categories II, III, or IV, these methods and workers must be approved by an independent third party under certain conditions.
Frequently Asked Questions
What takes place in ISO 9606-1 welder test?
The welder carries out a specific practical weld under certain conditions. After this, the test piece is inspected using the respective method, and the result is evaluated in accordance with relevant acceptance criteria.
What documentation should be provided for ISO 9606-1 welder test?
The testing scheme involves the relevant welding procedure specification, the test conditions and the necessary information for the identification of the welder and test piece. The total documentation which needs to be provided depends on the certification or examining scheme.
Is it possible for a welder to pass the test for both plates and pipes?
It depends on the qualification scheme. The plate and pipe are considered different types of products in ISO 9606-1, therefore, the resulting qualification needs to be verified in terms of the requirements of the intended production.
Will a 6G test make a welder qualified for all welding positions?
Not necessarily. The resulting qualification range needs to be verified in terms of the welding positions involved in the respective requirements. It would be wrong to interpret the 6G test as universal qualification automatically.
Which welding tests are used to prove the skill of a welder?
Depending on the test scheme, the inspection may include the visual test and other methods, such as the radiographic test, bend test, fracture test, macroscopic inspection, etc. The particular combination depends on the test piece.
Conclusion
The ISO 9606-1 welding qualification test is a clear, hands-on test that shows a welder’s ability to do the job properly, not just how much experience they have.
The process begins by figuring out what’s needed for production, choosing the right welding settings, and getting ready with the test piece.
Then, the welder does the actual welding and the test piece is checked and evaluated.
The two images in this article show the process from two different angles.
The first image uses an infographic to explain the steps of the certification process, while the second image shows the entire process as a timeline, starting from the production needs all the way to the qualification result.
For manufacturers and welding companies, the main idea is straightforward:
A welder shows their skill in real conditions, the test piece is checked, and if it works, that becomes their certified range of qualifications.
Ready for ISO 9606-1 Welder Qualification?
First Welding Certification Pvt Ltd (PRVÁ ZVÁRAČSKA,a.s.) carries out welder qualification processes based on international welding standards and certification rules.Make sure your welders’ qualifications meet the needs of your production work.