EN 1090
COMPLIANCE
ELEMENTS
EN 1090 WPS & WPQR Requirements: Ensuring Welding Quality and Compliance
By Technical Editorial Team
9 Min Read
10 Aug 2026
Table Of Contents
- Introduction
- Scope and Applicability
- WPS Content and Mandatory Fields
- WPQR Purpose, Tests, and Acceptance Criteria
- Welder Qualification and WPQ
- Documentation, Retention and Traceability
- Audit Checklist & Common Nonconformities
- WPS & WPQR Templates (Examples)
- Process Flow and Timeline
- Key Compliance Tips
- Standards Clause Comparison
- Conclusion
- Audit Checklist (WPS/WPQR focus):
Key Takeaways
Documentations
Process Flow
Tips
Checklist
Introduction
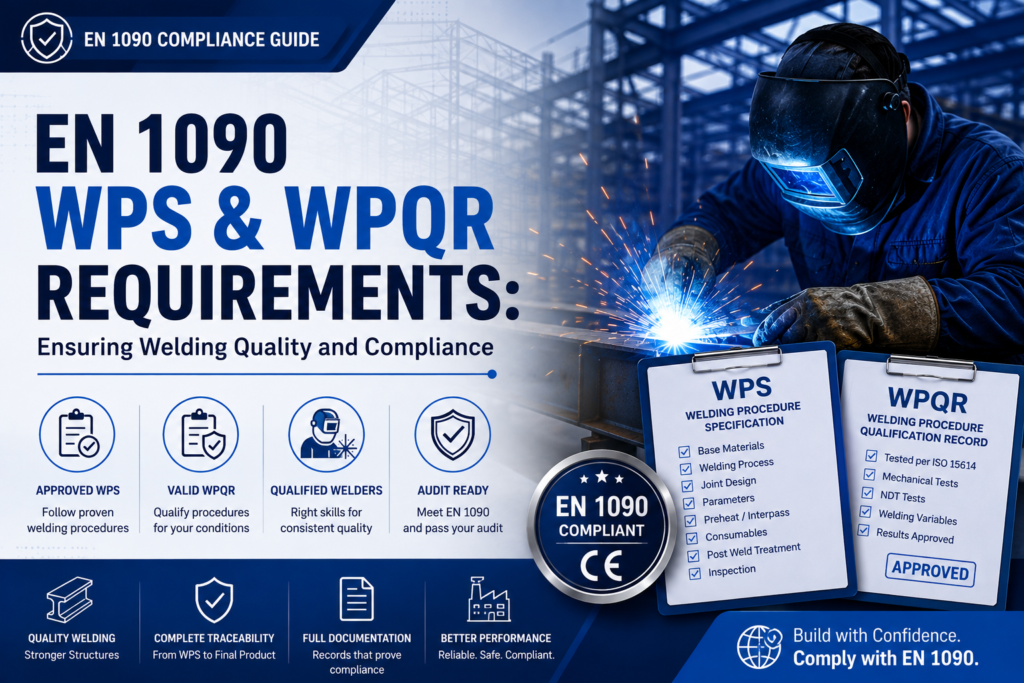
In EN 1090, which is the standard for the CE marking of steel structures, controlling the welding process is very important.Manufacturers need to write down Welding Procedure Specifications (WPS) and back them up with proper Welding Procedure Qualification Records (WPQR).A WPS is an approved way of welding that explains how to do the job, including the base metal, the filler material, and the welding parameters, among other things.The WPQR, also known as WPAR, is proof that this method has been tested and approved.Welders themselves also need to be qualified according to ISO 9606-1, which covers the welding process, the materials used, and the position of the weld.Under EN 1090-2, structures that are classified as EXC2, EXC3, or EXC4 need to have written and approved welding procedures, often following ISO 15614-1.This article covers the scope, definitions, what goes into a welding procedure, the tests needed, how to accept the work, how to document everything, and where to check for compliance.It uses official standards like EN 1090-1 and EN 1090-2, ISO 15614-1, ISO 9606-1, ISO 3834, and guidance from PZVAR to give a thorough and useful guide.
Scope and Applicability
EN 1090-1 and EN 1090-2 apply to steel and aluminum structures that are marked with the CE symbol.In the EU, any structural steel fabrication must follow the welding rules set in EN 1090-2 for steel or EN 1090-3 for aluminum.These standards set execution classes (EXC1 to EXC4), which are based on the level of risk.The higher the class, the stricter the welding and quality control requirements.From EXC2 onwards, which is the standard quality level, up to EXC4, which is the highest risk, both the Welding Procedure Specification (WPS) and Welding Procedure Qualification Record (WPQR) are required.It’s worth noting that EN 1090-2 allows for a simpler WPQR package for EXC2 or lower, but full procedure qualification is needed for EXC3 or EXC4.EN 1090-1 requires a Factory Production Control (FPC) system with documented procedures.This system includes welding coordination and quality control, following ISO 3834 guidelines.In summary, any steel project that falls under the EN 1090 scope needs a certified welding quality management system.This includes written WPSs with WPQRs, qualified welders, tracking of welding parameters and materials, and keeping of records.
Key Definitions
– Welding Procedure Specification (WPS): This is an approved welding method that outlines all the steps, parameters, and conditions needed to weld a joint.
It’s like a “recipe” that tells welders how to perform the job (including base metals, joint details, process, filler metal, current, shielding gas, preheat and interpass temperatures, travel speed, and other factors).A WPS is often first created as a preliminary WPS (pWPS), which is used during the procedure qualification.
– Welding Procedure Qualification Record (WPQR or WPAR): This is the proof that a WPS is valid.
It records the procedure qualification test (WPQT), including the actual parameters used and the results of the test.It shows that the welding method produces good quality welds.The WPQR is produced after destructive and non-destructive testing of a test coupon, as outlined in ISO 15614-1, and is usually checked and signed off by an independent examiner.
– Welder Performance Qualification (WPQ or Welder Certificate): This is a record that confirms a welder can perform quality welds under specific conditions, following ISO 9606 for steel or ISO 14732 for non-consumable or TIG welding.
ISO 9606-1 certificates specify the process, position, thickness range, and type of material the welder is qualified for.A welder must be qualified for the specific WPS they are using; they must re-qualify if they don’t use the process for more than six months.
– Execution Class (EXC1 to EXC4): This refers to the risk category of the structure, determined by the designer.
A higher EXC means stricter welding and quality control requirements.For welding, EXC2 (standard) and above require proper WPS and WPQR documentation, and typically follow ISO 3834 quality levels (EXC2 corresponds to ISO 3834-3, while EXC3 and EXC4 follow ISO 3834-2).
WPS Content and Mandatory Fields
A WPS that follows the rules must include all the important details needed for the welding process.Even though EN 1090 doesn’t list every detail, it refers to welding standards like ISO 15607 and ISO 15609 for how the WPS should be written.In real use, a WPS usually includes these minimum details:
– The type of joint (like the kind of weld, shape of the groove, use of backing), and the welding position (like flat, horizontal, vertical, or overhead)
– The base metal (like the steel grade or ISO 15608 P-number/group) and the thickness range
– The welding method (like GMAW or SMAW) and key settings (like current and voltage ranges, travel speed, and heat input)
– The type of filler metal (such as an electrode or wire, like ER70S-6) and the shielding gas (like type and flow rate)
– Electrical setup (like AC or DC, and polarity if needed) and preheat or interpass temperatures
– Whether any heat treatment after welding is needed
– The welder’s name and their qualification details (since the WPS is linked to a qualified welder)
– A reference to the standard that was used and the conditions that were tested (often a summary of the WPQR)
By having all this information, the WPS sets the exact method that was tested and approved.
The PZVAR guide says that the WPS gives everyone the same instructions, so each weld is done the same way every time.For example, it ensures that one welder doesn’t use a different electrode or position than another, which could lead to different weld quality.
Also, EN 1090-2 section 7.4.1 says that the WPS has to follow the procedure approved by the WPQR.
If any of the important details change, like the steel type, thickness outside the approved range, a new welding method, or a different filler metal, a new procedure qualification is needed.ISO 15614-1 Annex B describes all the rules for these important details.Manufacturers should record the exact ranges used in the WPQR and make sure the actual WPS stays within those limits.
WPQR Purpose, Tests, and Acceptance Criteria
The WPQR (or WPAR) is created by doing a Welding Procedure Qualification Test (WPQT) as per EN ISO 15614-1 for steel.It shows that the WPS can produce good welds.Here are the main points:
Purpose: The WPQR shows that a welding procedure was tested and approved.
It backs up the WPS by recording the original WPS used and the test results.
Testing: The WPQT involves welding a sample piece with the proposed WPS, then checking it using required non-destructive and destructive tests.
Non-destructive testing includes visual checks, checking for cracks (using methods like MT or PT), and 100% volumetric inspection (using RT or UT) for butt welds.Destructive tests may include: transverse tensile tests (with two samples, per ISO 4136), bend tests (face, root, and side bends, per ISO 5173), macro-etch tests (per ISO 17639), hardness tests (per ISO 9015 if needed by the material), and Charpy V-notch impact tests (per ISO 148 for low-temperature or high-strength steels).The exact tests depend on the product standard; EN 1090-2 refers to ISO 5817 and usually defaults to Level B (a strict standard) for qualification pieces.
Acceptance Criteria: All tests must meet the standards given in the relevant documents.
For instance, how good the weld is and the limits for defects depend on ISO 5817.If any test doesn’t meet the criteria, the WPS needs to be changed (like using a different filler or heat input) and tested again.
WPQR Documentation: The result is the Welding Procedure Approval Record (WPAR/WPQR), which must include: the original WPS used, all welding parameters that were actually used, and all test certificates and reports that can be traced back to the weld samples.
It should also list the range of what it’s qualified for, like thickness and material types, based on test results and ISO 15614 rules.An independent reviewer must look at the WPQR and sign it – EN ISO 15614-1 says that self-certification is not allowed for CE projects.
In short, the WPQR proves that the WPS is good.
Both documents need to be kept together: the WPS for daily work and the WPQR as proof it’s qualified.ISO 3834-2 also says that all production WPS must have a matching WPQR in the right range and that the qualification process should stay consistent.PZVAR stresses this: “A WPS must be connected to a qualified WPQR as required by the relevant code.” Without a WPQR, there’s no valid WPS and no compliant welding.
Welder Qualification and WPQ
Welder qualification, also known as Welder Performance Qualification or WPQ, is different from procedure qualification.According to EN 1090-2 §7.5, welders must be certified under EN ISO 9606-1 for steel or ISO 14732 for TIG and NDT operators, based on the processes and positions they use.In practice, this means each welder needs a current ISO 9606-1 certificate that covers the welding process, base material group, joint type, and welding position.
ISO 9606-1 sets out the approval levels for the certificate, including the process, thickness, diameter, positions, and material groups.
For instance, a test weld on a plate for a butt joint qualifies the welder for thicknesses ranging from 3 mm up to twice the test thickness.It is the manufacturer’s responsibility to make sure that every weld in production falls within a qualified range.If a joint is outside this range, or if the welding process changes (an essential variable), the welder must re-qualify.PZVAR points out that welder qualification and procedure qualification are separate: a skilled welder still needs an appropriate WPS/WPQR, and the same goes the other way around.
Also, EN ISO 14731 requires a Responsible Welding Coordinator (RWC) for projects rated EXC2 and above.
The RWC, often the Quality Manager or Lead Engineer, is responsible for managing the welding program, WPS/WPQR records, welder qualifications, NDT planning, and more.Their qualification, as per ISO 14731, depends on the EXC rating and materials used.While not a procedure itself, having a qualified RWC and clearly defining their responsibilities is a requirement for audits, as noted by PZVAR and EN 1090-2.
Documentation, Retention and Traceability
Under EN 1090, every weld needs to be linked back to its WPS or WPQR, the materials used, and the qualification records.EN 1090-1, sections 6.3.5 to 6.3.7, say that material certificates and inspection records must be kept.EN 1090-2, section 7 and Annex D, require that production details are recorded and stay within the WPS limits.In real practice, manufacturers use welding logbooks to track each weld by ID, the WPS used, the welder’s ID, heat numbers, preheat and interpass temperatures, and the results from non-destructive tests.
These records must be kept for a long time.
The Construction Products Regulation (EU) requires that the Declaration of Performance, FPC records, and important documents are kept for at least 10 years.EN 1090-1 also expects all FPC records, including WPS and WPQR, to be kept for about a decade.ISO 3834-2 also says welding records like certificates, logs, and WPQR must be kept for the length of the contract.
Therness (2025) explains that each weld must be traceable to its WPS, WPQR, the materials used, the welder, and the inspection results.
They suggest using clear IDs and time stamps to help with this.PZVAR’s checklist also says that not being able to trace materials (like mill certificates or batch IDs) or losing weld records is a big issue during audits.In short, having full documentation for each weld is key to staying compliant.
Audit Checklist & Common Nonconformities
PZVAR and industry guides point out similar issues that come up during audits.From their experience, common problems include:
– Missing or incomplete WPS/WPQR: Auditors often find that there is no formal WPS, or the WPS doesn’t have a valid WPQR.PZVAR clearly states: before an audit, you must check that you have approved WPS documents and valid WPQR records.Using an outdated or unapproved WPS is a major finding.
– Unqualified welders: Welder certificates (ISO 9606) that have expired or are incomplete are common.
If a welder’s WPQ is expired or doesn’t cover the actual welding process or position, then the welds they do are questionable.
– Missing parameter records: For EXC3/4, EN 1090 auditors require that every weld has recorded actual values like current, voltage, heat input, preheat, and interpass (as outlined in EN 1090-2 Annex D). If these aren’t recorded or verified (like saying “preheat assumed” instead of measuring it), it leads to findings.
– Incomplete NDT/inspection reports: If there are no records of NDT, auditors treat it like it never happened.
Missing radiography reports, MT/PT reports, or calibration certificates often show up.
– Weak welding coordination: If there is no qualified welding coordinator assigned or if responsibilities aren’t clear, auditors will point this out. EN 1090-2 (and ISO 3834) require a clear structure for welding management.
– General FPC issues: While audits focus on WPS/WPQR, they also look at factory production control.
Missing FPC manuals, no internal audits, or no corrective action systems are common issues.PZVAR’s “Scorecard” shows WPS/WPQR, material traceability, and welder qualifications as key areas.
To prepare, PZVAR recommends a thorough pre-audit review: make sure every production WPS has a corresponding WPQR, all welder certificates are up to date, NDT plans and results are stored, and the welding coordinator has clearly defined duties.
A simple audit checklist could include:
– Approved WPS with defined scope (material type, thickness, welding positions, etc.).
– Valid WPQR(s)/WPAR(s) that cover each WPS (with independent exam approval).
– Current ISO 9606-1 welder and operator certificates for every welding process used.
– A welding coordinator assigned (as required by EN 1090-2 §4 and ISO 14731) with proper qualifications.
– All welding parameter logs (preheat, current, heat input) and NDT reports for each weld.
– Material certificates (mill test reports) and batch traceability records.
– Up-to-date CE documentation (DoP, Control Plan) and FPC Manual (with 10-year retention).
Meeting these requirements will help avoid major non-conformities that can delay certification.
WPS & WPQR Templates (Examples)
Even though each company’s WPS and WPQR forms may look a bit different, they usually follow similar structures.
A typical WPS template, whether in Word or PDF, should have sections for the company name, WPS ID, title, welding process, type of base metal (like its specification or group), thickness range, joint design, welding position, filler metal type and grade, shielding gas used, electrical settings (such as amperage and voltage), preheat and interpass temperatures, heat input, post-weld treatments, and a reference to the qualified range (like from a WPQR).
It also needs approval details, such as signatures and dates.For example, Magmaweld’s guidelines mention method, metals, joint type, position, filler, gas, electrical settings, interpass temperatures, and heat input as the minimum required sections.
A standard WPQR template should include the WPQR ID, the reference to the pWPS ID, the test date, details about the base metal group and thickness, joint type, the welding process and actual parameters used, shielding gas, filler metal used, lab or CU numbers, and a list of destructive tests with results (such as pass or fail and measurements).
It should also include NDT reports (like RT, UT, MT, or PT), and the names and signatures of the welding supervisor, examiner, and laboratory.The document should end with the qualified range (based on ISO 15614 annex B) and a statement of approval.PZVAR suggests that a typical package includes the preliminary WPS, material details, welding settings, test results, NDT reports, lab findings, the WPQR itself, and the final production WPS.
Sample files: We have provided downloadable templates for a WPS and a WPQR in both Word and PDF formats.
These templates include all the fields mentioned above and are editable.You can download the WPS Template (Word) and the WPQR Template (Word).PDF versions are also available using the same links or by printing to PDF.
Process Flow and Timeline
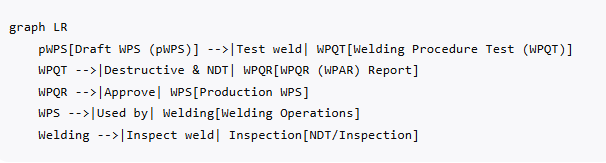
A simple process flow for approving a welding procedure is shown here (as illustrated by a Mermaid diagram).
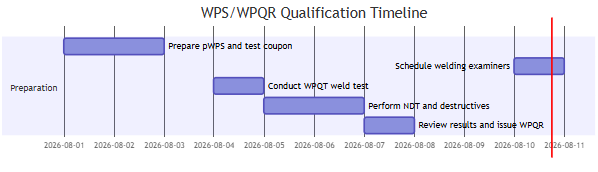
And a typical timeline for a WPQR:
Key Compliance Tips
Plan early: Don’t wait until the last minute to handle WPS or WPQR.PZVAR warns that an entire project can be delayed if the welding procedure isn’t properly approved.Start by preparing the pWPS and scheduling WPQT before you begin fabrication.
Match standards: Always use the most recent applicable standards.
EN 1090-2 refers to ISO 15614-1 for WPQTs, so make sure your testers and welders follow that standard for steel work.Similarly, ISO 9606-1 (the latest version) is the standard for welder testing.
Control essential variables: Before testing, double-check all the ranges in ISO 15614-1 Annex B.
Common mistakes happen when limits like the type of material (plate vs.pipe) or minimum preheat are overlooked.
Record actuals: Keep track of the real welding parameters used, not just what’s written on the plan.
The WPQR must include the actual amperage, voltage, and heat input used.Auditors often find missing or copied data; it’s best to use automated data capture for welding.
Organization: Keep a well-organized “Welding records” folder or database.
Link each WPS and WPQR to the welders and inspectors involved.Like ISO 3834, every weld should have a record of who did it, which procedure was used, which certificate it’s based on, and which test or inspection it went through.
Audit readiness: Use PZVAR’s audit checklist as a guide.
Do an internal mock audit that focuses on welding, checking WPS, WPQR, weld logs, and certifications.This can help find problems early.Fix any issues right away—like missing WPQRs, requalifying welders, or providing extra training if needed.
Standards Clause Comparison
The table below shows how the EN 1090 clauses match up with ISO welding standards and PZVAR guidance.
| Requirement | EN 1090-1 | EN 1090-2 | ISO 15614-1 | ISO 9606-1 | ISO 3834 (Welding QA) | PZVAR Guidance |
|---|---|---|---|---|---|---|
| WPS documentation | §6.3.1 FPC – document procedures (incl. welding) | §7.4 – WPS must be validated by procedure test | (ISO 15607 governs WPS format; ISO 15609 series) | – | Requires documented WPS for all production welds | “Approved WPS documents” must be available |
| WPQR (procedure qual.) | (FPC manual should reference WPS testing) | §7.4 – WPS qualified per EN ISO 15614‑1 | Defines the procedure qualification test, required NDT/mechanical tests and WPAR content | – | WPQR (PQR) required to prove WPS; independent approval | “Valid WPQR documentation” must be available |
| Welder qualification | (FPC should ensure trained personnel) | §7.5 – Welders must be ISO 9606‑1 qualified | – | Specifies welder test and range of approval | Requires certified welders per ISO 9606-1 | “Current welder qualification certificates” required |
| Parameter control | §6.3.3 – equipment calibration; §6.3.6–6.3.7 – inspection plan | §7 & Ann D – All weld parameters kept within WPS limits during production | Requires actual parameters be recorded in WPAR/WPQR | – | ISO 3834-2 requires monitoring of welding parameters (heat input, preheat) | Welding logs (parameters, NDT) should be documented |
| Material traceability | §6.3.5 – record mill certs/IDs (FPC) | §12 – traceability of steel/al parts, certificates | (Traceability to test pieces, but mostly product standard) | – | Requires linking each weld to material certs | Maintain material certificates and IDs (heat numbers) for audit |
| Records & retention | §6.3.8 – procedures for non-conformities; CPR Art.11 – keep DoP/records 10+ years | (Audit file of WPQR/WPS should be kept) | WPAR has no expiry if in use; must be retained (no auto-reset) | – | ISO 3834-2: keep all welding records per contract (often 10 years) | Keep all WPS, WPQR, qualification and inspection records for 10+ years |
Conclusion
Implementing strong WPS/WPQR controls is essential for following EN 1090 standards.All CE-marked welded parts must be made using a tested procedure, with proper records and trained workers.By following the steps like writing a WPS, doing WPQR tests as per ISO 15614-1, certifying welders under ISO 9606-1, and keeping detailed records, manufacturers can make sure their welding is up to standard and easy to check.As PZVAR points out, treating WPS and WPQR as key parts of the quality system helps keep welds consistent, makes certification smoother, and reduces the need for fixes later.
Audit Checklist (WPS/WPQR focus):
– Approved welding procedures (WPS) with clear details about the materials, thickness, welding position, and process.
Each WPS has a corresponding WPQR or WPAR, checked by qualified examiners.
– Welders have ISO 9606-1 certificates that cover all the welding jobs they are doing now.
– A Welding Coordinator (RWC) is assigned, and their job duties are clearly set according to EN 1090-2.
– The real welding settings used by the welders are recorded and checked against the WPS, including preheat, interpass, and heat input.
– Every weld has a full NDT or inspection record linked to it.
– Material certificates and batch numbers can be traced back to each weld.
– All documents like WPS, WPQR, certificates, and reports are kept in order and stored for at least 10 years.
Following this guide helps quality managers and engineers understand the EN 1090 welding rules and be ready for certification checks.