ISO 9606-1
WELDER QUALIFICATION
GUIDE
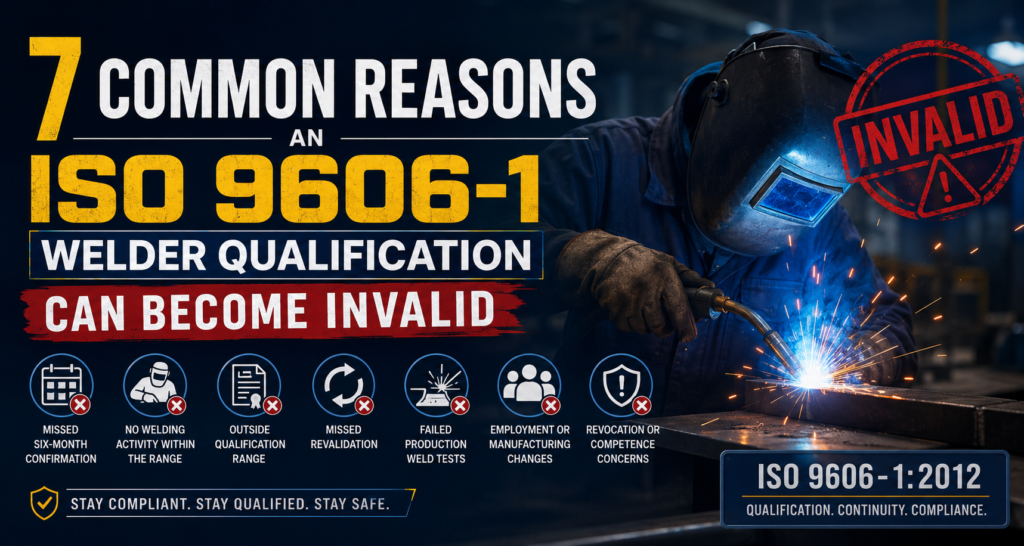
7 Common Reasons an ISO 9606-1 Welder Qualification Can Become Invalid
By First Welding Certification Technical Editorial Team
9 Min Read
22 Aug 2026
Table Of Contents
- What Does It Mean When an ISO 9606-1 Qualification Becomes Invalid?
- 1. Missing the Six-Month Confirmation
- 2. The Welder Stops Welding Within the Qualified Range
- 3. Welding Outside the Approved Qualification Range
- 4. Missing the Required Revalidation
- 5. Required Production Welds Fail Examination
- 6. The Welder's Employment or Manufacturing Conditions Change
- 7. The Qualification Is Revoked or There Is a Valid Reason to Question the Welder's Ability
- Invalid Qualification vs. Qualification Outside Its Range
- How to Check Whether an ISO 9606-1 Welder Qualification Is Still Valid
- ISO 9606-1 Welder Qualification Validity Checklist
- How Manufacturers Can Prevent ISO 9606-1 Qualification Problems
- Final Takeaway
- Frequently Asked Questions
Key Takeaways
Identify audit requirements before assessment
Review welding procedures and quality records
Verify personnel competence and qualifications
Maintain consistent welding quality and traceability
An ISO 9606-1 welder qualification is not just a certificate that stays valid until the date it says.Its validity depends on regular checks, ongoing welding work, staying within the approved range of welds, and meeting any revalidation rules.
This is one of the most common areas of confusion during welding audits.
A welder might have a certificate that looks like it’s still valid, but the qualification could no longer be acceptable for production work. This can happen if the required six-month confirmation wasn’t done, the welder stopped doing the qualified work, or the revalidation conditions weren’t met.
ISO 9606-1:2012 sets the rules for welders who do manual or partly mechanized fusion welding on steel.
It uses specific essential variables to determine the qualification, meaning the qualification only covers the welding conditions and ranges that were tested.
This guide covers seven common reasons why an ISO 9606-1 welder qualification might become invalid, along with what manufacturers, welding coordinators, and quality teams can do to avoid these issues.
Related guide: For a full explanation of qualification validity, six-month continuity, renewal options, and qualification ranges, see the PZVAR pillar article: ISO 9606-1 Welder Qualification: Validity, Continuity & Renewal Explained (2026).
What Does It Mean When an ISO 9606-1 Qualification Becomes Invalid?
Under ISO 9606-1, a welder’s qualification stays valid only if it is regularly checked.
The standard has a clear way to check this every six months.
This check makes sure the welder is still working within the range they were qualified for.If this check isn’t done, the qualification is no longer valid.
It’s important to understand two things that are often mixed up:
- Certificate validity: This means whether the qualification is still officially recognized.
- Qualification range: This means whether the welder is allowed to do the specific welding job they are asked to do.
A certificate can still be valid even if it doesn’t cover a certain weld, because the process, material, thickness, position, or another important factor is outside what was approved.
ISO 9606-1 says that if welding is needed outside the approved range, a new qualification test is required.
1. Missing the Six-Month Confirmation
The main reason an ISO 9606-1 qualification stops being valid is because the welder doesn’t complete the six-month confirmation that’s needed.
The standard says that every six months, the welder’s qualification must be checked by the person in charge of welding or by the examiner.
This check ensures that the welder has been working within the range of their qualification during that time and allows the qualification to stay valid for another six months.
Why is this important?
A company might look at the original certificate and see a future expiry or revalidation date.
But just seeing that date isn’t enough.
The six-month confirmation is something that needs to be done regularly.
For example:
– Qualification test completed: January 2026
– First confirmation: July 2026
– Second confirmation: January 2027
– Third confirmation: July 2027
If the required confirmation isn’t done on time, the qualification might become invalid even if the full revalidation period hasn’t ended yet.
Common audit issue
A company may have a certificate that looks valid, but they can’t show proof of the six-month confirmation.
Because of that, an auditor might question whether the welder was actually qualified when they made certain welded parts.
How to avoid this problem
Keep a welder continuity register that includes:
– Welder’s name or ID
– Certificate number
– Welding process used
– Date of qualification
– Dates of six-month confirmations
– Name and signature of the person responsible
– Evidence that welding work was done
– Details of the qualification range
Using a digital reminder system can also help ensure that confirmation dates are not missed.
2. The Welder Stops Welding Within the Qualified Range
A qualification shows that a welder has the right skills and experience for a specific type of welding work.
If a welder stops doing that type of welding, the company might not have proof that the welder is still qualified.
This is especially important if a welder is away from welding for a long time and does things like:
– Working in a different part of the company
– Doing inspections
– Handling non-welding tasks
– Doing administrative work
– Using a different welding method
– Not being at work
– Waiting for a project to start again
The six-month confirmation isn’t just a signature.
It’s meant to show that the welder actually did the welding work they’re qualified for.
For example, if a welder is trained for process 111 and usually does SMAW welding, but then works on inspections and preparation for eight months without doing any of that welding, just signing the certificate later won’t prove that the welding was done.
Before the welder goes back to welding, the qualification should be checked again.
Best practice is for companies to keep clear records that show qualified welders actually did the welding.
Useful records include:
– Weld maps
– Weld reports
– Welder ID numbers
– Production logs
– Job cards
– Inspection reports
– NDT reports
– Weld traceability records
3. Welding Outside the Approved Qualification Range
This situation is a bit different from a qualification that has expired.
The certificate might still be valid, but the welder might not be qualified for a specific production weld.
ISO 9606-1 explains what qualifications cover through essential variables.
These include:
– The welding process used
– The type of product being welded
– The kind of weld
– The group of filler material
– The type of filler material
– The thickness of the material
– The outside diameter of the pipe
– The welding position
– Details about the weld, like whether it uses backing or is done from one or both sides
If the production conditions are outside the range covered by the qualification, a new test might be needed.
Example:
Imagine a welder is qualified for:
– Process: 111
– Product: plate
– Weld type: butt weld
– Material: a specific group of qualified materials
– Thickness: within the approved range on the certificate
– Position: within the tested range
This same welder can’t automatically be used for every steel welding job.
For instance, if the job involves:
– A different welding process
– An unqualified material group
– A different type of weld
– A thickness outside the approved range
– A position that wasn’t tested
– A different filler material category
Then the production weld might be outside the certificate’s qualification range.
The key lesson is:
A valid certificate doesn’t mean the welder is allowed to do any type of welding.
Before assigning a welder to a production job, the welding coordinator should check the job requirements against the welder’s qualification certificate.
4. Missing the Required Revalidation
ISO 9606-1 offers various ways to revalidate a welder’s qualification.
The method used is listed on the certificate when the qualification is first given.
Some common options include:
Route 9.3(a): Retesting
The welder has to take a new qualification test at the required time interval.
Route 9.3(b): Production Weld Testing
The qualification can be revalidated by testing specific production welds made during the relevant time period.
The standard says that two welds made in the last six months of the qualification’s validity period should be tested.These welds need to be properly examined and the results must be recorded.
Route 9.3(c): Continued Validity under Certain Conditions
This route allows the qualification to remain valid if certain conditions set by the standard are met, such as the manufacturer’s requirements, the welding quality system in place, and documented evidence of acceptable welding performance.
Why companies face problems
A manufacturer might think that all ISO 9606-1 certificates follow the same renewal process.
This is not true.
The correct revalidation method must be checked on the actual certificate and compared with the requirements of the certification or examining body.
Best practice
Before the revalidation date:
– Check the method listed on the certificate.
– Find out who the responsible examiner or examining body is.
– Review the necessary production records.
– Make sure the required welds can be traced back to the welder.
– Arrange for testing if needed.
– Record the outcome of the revalidation.
– Update the welder qualification register.
5. Required Production Welds Fail Examination
For companies that use a production-weld-based revalidation method, the quality of the chosen welds is very important.
If the chosen route requires production welds to be checked, those welds must meet the necessary acceptance standards.
For example, Route 9.3(b) requires testing two production welds that were made during the last six months of the revalidation period.
The results of these tests must be kept on record, and the welds must meet the required acceptance criteria.
If the required production welds:
– Don’t pass the required inspection,
– Can’t be linked to a qualified welder,
– Don’t match the needed welding conditions,
– Are not well-documented, or
– Can’t show that they meet the revalidation requirements,
Then the revalidation might not be successful.
Why traceability is important
Just saying “This weld was made by a qualified welder” isn’t enough.
The company needs clear, objective proof that connects the production weld to the welder.
Depending on how the company’s system works, this could include:
Welder ID → Weld number → WPS → Material → Joint → Inspection or NDT report
This chain of traceability is very useful during an audit.
6. The Welder's Employment or Manufacturing Conditions Change
Changes in how someone works or how a product is made can cause issues, especially when the ongoing validity of a qualification depends on conditions connected to the manufacturer.
This is especially important when using the continuous-validity route.
Under Route 9.3(c), the welder must continue working for the same manufacturer that originally issued the qualification.
Also, other requirements related to the manufacturer’s welding quality system and documented acceptable welding performance must be met.
Example:
A welder gets a qualification while working for Manufacturer A.
Later, the welder moves to Manufacturer B.
Manufacturer B can’t just assume the qualification is still valid under the same continuous-validity setup.
The conditions on the certificate and the requirements from the certification body need to be checked again.
Other changes that require a review include:
– Changing employers
– Moving to another manufacturing company
– Major changes in welding tasks
– Losing or changing the quality-system certification
– Changing the certification arrangement
– Changing the organization responsible for exams or certifications
Important point:
Just because a welder changes jobs doesn’t mean all their qualifications are automatically invalid.
The right approach is to review the qualification route, certificate conditions, and the relevant certification scheme instead of making assumptions.
7. The Qualification Is Revoked or There Is a Valid Reason to Question the Welder's Ability
ISO 9606-1 also has a specific rule about removing a welder’s certification.
This is important because keeping a certificate valid is more than just checking dates and paperwork.
A certification system needs to handle situations where there is a real reason to doubt if a welder still has the needed skills.
For example, a company might notice a repeated and serious drop in the quality of the welds, which shows the welder may not be able to consistently make good welds.
In these cases, the company shouldn’t just use an old certificate and keep the welder working on important projects.
What should the company do?
If there is a real concern:
Stop and look into the problem.
Check the welder’s recent work records.
Look at the actual welds and test results.
Review the welding procedure and conditions used.
Find out if the problem is with the welder, the method, the materials, or the equipment.
Talk to the welding coordinator or examiner in charge.
Follow the right steps to recheck the welder’s skills.
Provide training or retest if needed.
The goal isn’t just to keep the certificate active.
The goal is to be sure the welder is still clearly able to do the job properly.
Invalid Qualification vs. Qualification Outside Its Range
This distinction is extremely important during audits.
| Situation | Certificate status | Can the welder perform that job? |
|---|---|---|
| Six-month confirmation missed | May become invalid | No, until status is properly resolved |
| Required revalidation not completed | May become invalid | No |
| Welder outside approved processes | Certificate may still be valid | No |
| Thickness outside qualified range | Certificate may still be valid | No |
| Position outside qualified range | Certificate may still be valid | No |
| Material group outside qualification | Certificate may still be valid | No |
| Production weld fails required revalidation testing | Revalidation may fail | No under that route |
| Certificate properly confirmed and job within range | Valid | Yes, subject to production requirements |
This is why simply checking the expiry date on a welder certificate is not sufficient.
How to Check Whether an ISO 9606-1 Welder Qualification Is Still Valid
Before putting a welder to work on an important welding task, follow this check process.
Step 1: Check the certificate
Make sure the certificate has:
– Welder’s name or ID
– Certificate number
– Qualification standard
– Welding process
– Material group
– Product type
– Weld type
– Thickness or diameter range
– Position
– Filler material
– Weld details
– Date of qualification
These are all set out in ISO 9606-1 as part of the qualification system.
Step 2: Check the six-month confirmation
Look for proof that the qualification was checked every six months.
Don’t just rely on when the certificate was first given.
Step 3: Check the real welding work
Ensure the welder has done welding within the range covered by their qualification.
Step 4: Check the revalidation method
Find out if the certificate uses:
– 9.3(a)
– 9.3(b)
– 9.3(c)
Then make sure all the needed steps for revalidation have been done.
Step 5: Compare the job with the certificate
Check the following:
– Process
– Product
– Weld type
– Material
– Filler
– Thickness or OD
– Position
– Weld details
If any of these key parts don’t match what’s allowed, send the job back for a qualification check.
Step 6: Check traceability
Ensure the welder’s work can be followed through the company’s records of production and inspection.
ISO 9606-1 Welder Qualification Validity Checklist
For manufacturers, welding coordinators, and quality managers, this easy checklist can help avoid common issues with weld qualifications:
– The certificate is available and can be read clearly
– The certificate number can be traced back
– The qualification standard is clearly stated
– The welding process used is the same as the one in production
– The material type is within the approved range
– The filler material is within the approved range
– The thickness or pipe size is within the allowed range
– The welding position is within the allowed range
– The type of weld is covered in the qualification
– All necessary weld details are included
– The six-month confirmation is up to date
– The welding work is properly recorded
– The path for revalidation is known
– All revalidation steps have been completed
– Each production weld can be linked back to the welder
There are no unresolved issues about the welder’s skills or experience
How Manufacturers Can Prevent ISO 9606-1 Qualification Problems
The best way is to treat welder qualification like a controlled quality record, not just a document that gets stored once certification is done.
A good system should have a central welder qualification matrix.
For each welder, keep track of:
| Record | Information to maintain |
|---|---|
| Welder identification | Name and unique welder ID |
| Certificate | Certificate number and issuing body |
| Process | 111, 135, 136, 138, 141, etc. |
| Material | Qualified material group |
| Product | Plate/pipe |
| Weld type | Butt/fillet |
| Thickness/OD | Approved range |
| Position | Qualified positions |
| Filler | Applicable filler group/type |
| Continuity | Six-month confirmation |
| Revalidation | 9.3(a), 9.3(b) or 9.3(c) |
| Evidence | Production and examination records |
| Status | Active / review required / expired |
This helps the welding coordinator decide if a welder is suitable for a certain job.
Final Takeaway
An ISO 9606-1 welder qualification can stop being valid for reasons that have nothing to do with the date on the certificate.
The seven most common reasons are:
– Not completing the six-month confirmation
– Not keeping welding work within the approved range
– Using the welder outside the approved qualification range
– Not following the required revalidation steps
– Failing production weld tests that are required
– Changes in the manufacturer or working conditions that affect how the qualification was obtained
– Revoking the qualification or having concerns about the welder’s ongoing skills
The main takeaway for manufacturers is simple:
Don’t just check the expiry date on the certificate.
Make sure to check continuity, the qualification range, the revalidation process, and traceability.
ISO 9606-1:2012 is still the latest published version as of 2026, though ISO is currently working on ISO/DIS 9606.2 as a new revision.
Companies should also keep an eye on updates from certification bodies and standards when maintaining their welder qualification system.
For a full explanation of how the six-month confirmation, revalidation, and qualification ranges work, continue with the PZVAR pillar article:
ISO 9606-1 Welder Qualification: Validity, Continuity & Renewal Explained (2026)
This supporting article should link back to the pillar using anchor text such as “ISO 9606-1 welder qualification validity”, “ISO 9606-1 qualification validity and renewal”, or “complete guide to ISO 9606-1 welder qualification validity.”
Frequently Asked Questions
Does an ISO 9606-1 certificate automatically remain valid until its expiry date?
No. The qualification is subject to the required six-month confirmation of validity. Missing the confirmation can cause the qualification to become invalid before the broader revalidation period is reached.
What is the six-month rule for ISO 9606-1?
The qualification must be confirmed every six months by the person responsible for welding activities or the examiner/examining body, confirming that the welder has worked within the qualification range.
Can a valid ISO 9606-1 certificate be used for every welding job?
No. The qualification only covers the applicable range established by the test. ISO 9606-1 defines essential variables including process, product type, weld type, filler material, dimensions, position and weld details.
Does changing welding process invalidate the certificate?
A change of welding process can place the work outside the existing qualification. ISO 9606-1 states that each test normally qualifies one welding process, subject to specific exceptions.
Can a welder's qualification become invalid because of a long break from welding?
A prolonged absence from the relevant welding activity can affect the ability to provide the required confirmation that the welder has worked within the qualification range. The qualification status should therefore be reviewed before the welder returns to production.
What happens if the required production welds fail during revalidation?
Where the selected revalidation route requires production weld testing, failure to satisfy the applicable examination and acceptance requirements can prevent successful revalidation. The qualification should then be handled according to the applicable certification procedure.
How can a company prevent welder qualification expiry?
Use a centralized welder qualification matrix, maintain six-month confirmation records, track revalidation dates, maintain weld traceability and compare every production assignment against the welder’s approved qualification range.