WPS & WPQR
Qualifications
Test Requirements
WPS and WPQR Qualification Tests: Complete Testing Requirements Guide
By First Welding Certification Technical Editorial Team
10 Min Read Time
22 Sep 2026
Table Of Content
WPS and WPQR Qualification Tests: Required Tests Explained
WPS
Welding Procedure Specification
Inspection
Visual and NDT examination
Mechanical Tests
Tensile, bend, impact & hardness
WPQR
Welding Procedure Qualified Record
Introduction
Welding procedure qualification is an important part of ensuring consistent weld quality in fabrication, manufacturing, construction, structural steel and other engineering applications. A WPS (Welding Procedure Specification) defines the welding variables and instructions used for production welding, while a WPQR (Welding Procedure Qualification Record) documents the results of the welding procedure test.
So, what tests are required for WPS and WPQR qualification?
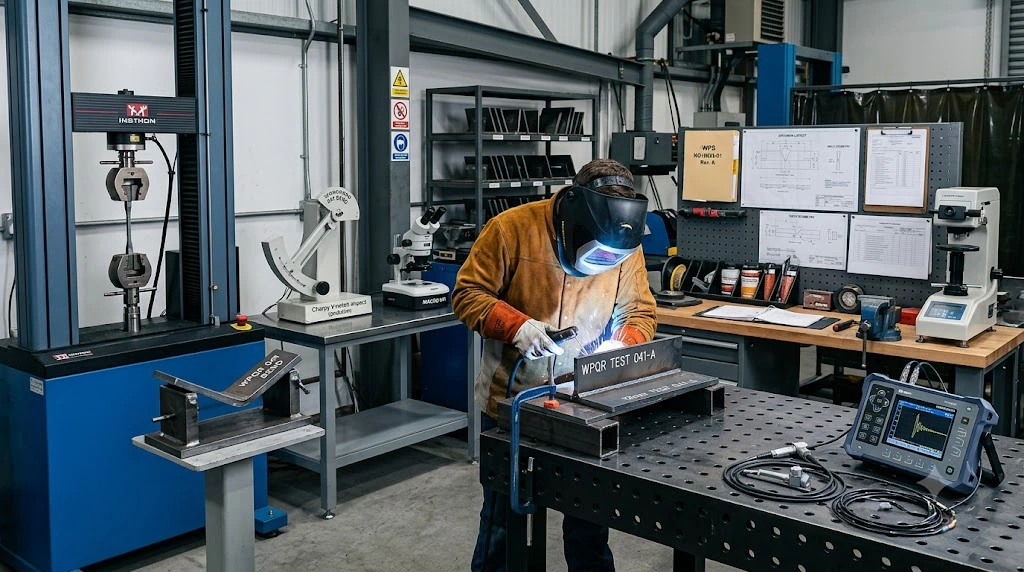
Depending on the applicable standard and qualification requirements, welding procedure qualification may involve visual examination, non-destructive testing (NDT), tensile testing, bend testing, impact testing, hardness testing and macro examination. The exact combination is not universal and depends on factors such as material, thickness, welding process, joint type, qualification level and project requirements.
For welding procedures covered by ISO 15614-1, the qualification process is based on welding procedure tests that demonstrate whether the proposed procedure can produce a welded joint with the required characteristics. ISO currently lists ISO 15614-1:2017 with Amendment 1:2019 as the published edition, while a draft replacement, ISO/DIS 15614-1, is under development.
What Are WPS and WPQR?
Before understanding the testing requirements, it is important to distinguish between WPS and WPQR.
WPS — Welding Procedure Specification
A WPS describes how a welding operation should be performed. Depending on the applicable standard, it can include information such as:
- Welding process
- Parent material
- Joint design
- Welding position
- Filler material
- Preheat temperature
- Interpass temperature
- Welding parameters
- Heat input
- Shielding gas
- Welding technique
- Post-weld heat treatment
A preliminary WPS, commonly called a pWPS, can be qualified through a welding procedure test.
WPQR — Welding Procedure Qualification Record
A WPQR records the actual welding variables and results obtained during the procedure test.
The record can include:
- Test piece details
- Material information
- Welding process
- Actual welding parameters
- Welder information
- Filler metal
- Preheat and interpass temperatures
- Examination results
- Mechanical test results
- Qualification range
In simple terms:
WPS = how the welding should be performed
WPQR = evidence that the welding procedure has been qualified
What Tests Are Required for WPS and WPQR Qualification?
There is no single test package that applies to every WPS or WPQR qualification.
The required examinations and tests depend on the applicable qualification standard and the specific welding application.
Common examinations and tests can include:
| Test / Examination | Main Purpose |
|---|---|
| Visual Examination | Checks visible weld condition and surface imperfections |
| NDT | Detects relevant surface or internal discontinuities |
| Tensile Test | Evaluates tensile performance of the welded joint |
| Bend Test | Evaluates ductility and weld integrity |
| Impact Test | Evaluates toughness where required |
| Hardness Test | Measures hardness across selected weld regions |
| Macro Examination | Examines weld cross-section and fusion characteristics |
The applicable standard, material, thickness, welding process, joint configuration and project specification should be reviewed before deciding the final test package.
1. Visual Examination
Visual examination is a fundamental part of weld inspection.
The completed test piece can be examined for visible conditions such as:
- Surface cracks
- Undercut
- Excessive reinforcement
- Weld profile
- Surface irregularities
- Visible porosity
- Incomplete or unacceptable weld appearance
Visual examination provides an initial assessment of the weld before additional testing is considered.
However, visual inspection cannot identify every internal or mechanical characteristic of a welded joint. Additional NDT or destructive testing may therefore be required.
2. Non-Destructive Testing
Non-destructive testing (NDT) examines a welded joint without destroying the test piece.
Depending on the applicable requirements, NDT methods may include:
Radiographic Testing — RT
Radiographic testing can be used to examine suitable welded joints for internal discontinuities.
Ultrasonic Testing — UT
Ultrasonic testing uses high-frequency sound waves to detect and evaluate discontinuities within suitable weld configurations.
Magnetic Particle Testing — MT
Magnetic particle testing is applicable to suitable ferromagnetic materials and can detect relevant surface and near-surface discontinuities.
Penetrant Testing — PT
Penetrant testing is used to identify surface-breaking discontinuities on suitable non-porous surfaces.
The applicable NDT method should be selected based on the governing qualification requirements rather than assuming that every WPQR requires all NDT methods.
3. Tensile Testing
A tensile test evaluates the mechanical performance of the welded joint under tensile loading.
A specimen is removed from the welded test piece and subjected to a controlled tensile test.
Depending on the applicable requirements, the test can provide information about:
- Tensile strength
- Failure location
- Welded joint performance
Tensile testing can demonstrate whether the qualified welding procedure produces a joint capable of meeting the specified mechanical requirements.
The applicable qualification standard determines the specimen requirements, testing method and acceptance criteria.
4. Bend Testing
Bend testing evaluates the ductility and integrity of a welded joint.
A prepared specimen containing the weld is bent according to the applicable test method. The bent specimen is then examined for relevant discontinuities.
Depending on the qualification requirements, different bend-test configurations may be applicable.
Bend testing is commonly associated with welding procedure qualification, but the required type and extent should always be determined from the applicable standard.
5. Impact Testing
Impact testing evaluates the toughness of a welded joint under specified conditions.
It becomes particularly relevant when the application requires impact toughness.
Impact requirements can depend on factors such as:
- Parent material
- Material thickness
- Material group
- Service temperature
- Application
- Applicable standard
Therefore, impact testing is not automatically required for every WPQR.
Where impact toughness is specified, the applicable test temperature, specimen requirements and acceptance criteria should be established before conducting the procedure test.
6. Hardness Testing
Hardness testing measures the hardness of selected areas of a welded joint.
Measurements can involve regions such as:
- Weld metal
- Heat-affected zone
- Parent material
Hardness testing can be relevant for specific materials, welding processes, thicknesses and applications.
The applicable qualification requirements determine whether hardness testing is necessary and how the measurements should be performed.
7. Macro Examination
A macro examination involves preparing and examining a cross-section of the welded joint.
It can provide information about:
- Weld penetration
- Fusion
- Weld profile
- Root condition
- Weld runs
- Internal weld geometry
- Visible imperfections
Macro examination provides a cross-sectional view of the weld and can be useful for assessing the physical characteristics of the completed joint.
Factors That Determine WPQR Testing Requirements
The required tests are not selected randomly. Several technical variables can influence the qualification requirements.
1. Parent Material
The material being welded can influence the applicable qualification requirements.
2. Material Thickness
The thickness of the test piece can affect the qualified range and applicable testing requirements.
3. Welding Process
Different welding processes have different qualification considerations.
4. Joint Type
Butt welds, fillet welds and other joint configurations can have different qualification requirements.
5. Welding Position
The welding position used during the procedure test can affect the resulting qualification range.
6. Impact Requirements
Applications requiring specified toughness can introduce impact-testing requirements.
7. Hardness Requirements
Certain materials and applications can require hardness measurements.
8. Applicable Standard
The governing welding qualification standard determines the framework for testing and qualification.
9. Qualification Level
ISO 15614-1:2017 defines two levels of welding procedure testing. Level 2 has a greater extent of testing and more restrictive qualification ranges than Level 1.
Therefore, the applicable qualification level should be established before preparing the final testing plan.
WPS to WPQR Qualification Process
The general workflow can be understood as:
- Define the welding application
- Prepare the preliminary WPS (pWPS)
- Select materials and welding variables
- Weld the procedure test piece
- Perform the required examinations and tests
- Evaluate the test results
- Record the results in the WPQR
- Establish the qualification range
- Prepare or finalize the qualified WPS
This process connects the proposed welding procedure with documented test evidence.
WPS vs WPQR
WPS and WPQR are closely related but serve different purposes.
| WPS | WPQR |
|---|---|
| Defines welding instructions | Records qualification test results |
| Used for production welding | Provides qualification evidence |
| Contains specified welding variables | Records actual variables used during testing |
| Guides welding personnel | Demonstrates procedure qualification |
| Applies within the qualified range | Establishes the qualification range |
pWPS → Welding Procedure Test → Examination & Testing → WPQR → Qualified WPS
For a detailed comparison, see our guide on WPS vs WPQR.
Frequently Asking Questions
What tests are required for WPS and WPQR qualification?
Depending on the applicable requirements, tests and examinations can include visual examination, NDT, tensile testing, bend testing, impact testing, hardness testing and macro examination. The exact combination depends on the standard and welding application.
Are all tests mandatory for every WPQR?
No. The required tests depend on the applicable standard, material, thickness, welding process, joint configuration, qualification level and project requirements.
Is tensile testing required for WPQR qualification?
Tensile testing can form part of the welding procedure qualification test requirements. The applicable standard determines when it is required and specifies the relevant testing conditions and acceptance requirements.
Is bend testing required for every WPQR?
Not necessarily. Bend testing requirements depend on the applicable qualification standard and specific welding procedure qualification conditions.
Which standard is used for welding procedure qualification?
For welding procedures covered by its scope, ISO 15614-1:2017 is the published ISO standard, with Amendment 1:2019. ISO is also developing ISO/DIS 15614-1 as a replacement. The applicable edition and project requirements should be verified before qualification.
Conclusion
WPS and WPQR qualification tests demonstrate whether a proposed welding procedure can produce a welded joint that meets the applicable requirements.
Depending on the qualification conditions, testing can involve:
- Visual examination
- Non-destructive testing
- Tensile testing
- Bend testing
- Impact testing
- Hardness testing
- Macro examination
However, not every WPS or WPQR requires every test. The final testing requirements should be determined from the applicable standard, material, thickness, welding process, joint configuration, qualification level and project specifications.
Understanding these requirements before welding the qualification test piece can make the qualification process more structured and reduce unnecessary testing or documentation issues.
Related Searches
- WPS & WPQR Explained: The Complete Manufacturer’s Guide to Welding Procedure Qualification, Requirements, Standards and Industrial Applications (2026)
- WPS vs WPQR: Understanding the Key Differences Every Manufacturer Should Know (2026 Guide)
- EN 1090 WPS & WPQR Requirements: Ensuring Welding Quality and Compliance
Need WPS/WPQR Qualification?
First Welding Certification Pvt. Ltd. (PRVÁ ZVÁRAČSKÁ, a.s.) works with welding certification requirements for industrial and manufacturing applications.
When preparing a WPS/WPQR qualification requirement, key details such as material, thickness, welding process, joint type, welding position and applicable standard should be identified before determining the appropriate qualification and testing requirements.