ISO 3834
RENEWAL
REASSESSMENT
17 Sep 2026
ISO 3834 Certification Renewal: When and How Should Welding Manufacturers Reassess Their Certification?
By Editorial Team
Table Of Contents
Related Blogs
SEP
15
Which Industries and Manufacturers Need ISO 3834 Certification in India and International Markets? Top 10 Sectors That Need It
SEP
12
Best Standard for Fusion Welding Quality Control: Why ISO 3834 Is Required for EN 1090 & EN 15085
SEP
08
ISO 3834 Latest Edition 2026: 2021 Revision, Current Status & What Welding Manufacturers Need to Know
AUG
24
ISO 3834 Certification Cost in India: Factors, Fees & Budget Guide
JLY
30
EN ISO 3834 Certification Requirements: What Welding Manufacturers Need to Know in 2026
See Also.....
Executive Summary: ISO 3834 certification usually happens over several years, with yearly checks and a full review at the end.For instance, many businesses use a 3-year certificate with audits in the first two years and a renewal in the third (some systems allow up to 5 years with yearly checks). Reasons for reassessing include big changes in products or processes, serious issues found during audits, new rules or standards, mergers or acquisitions, or changes in the supply chain. To prepare for renewal, companies should do detailed internal checks and management reviews, fix any problems, and maybe do a pre-check before the official second stage audit. Typical issues found during audits are missing records of welders, WPSs not available at workstations, poor tracking of materials, and repairs that aren’t documented. To stay ready, manufacturers must keep full welding records like WPSs, PQRs, welder and NDT certificates, material certificates, and inspection reports. They should also have an active system for fixing problems. Important performance measures like weld acceptance rate, rework ratio, internal audit results, and how quickly CAPA issues are solved should be tracked monthly or quarterly and discussed in management meetings. This guide covers the basics of ISO 3834, its scope, timelines, reasons for reassessment, steps for renewal, common issues and how to fix them, checklists for resources, key performance indicators, and real examples.
ISO 3834 Overview: Parts, Scope & Applicability
ISO 3834 is a set of standards that set quality rules for welding metal. It’s not the same as ISO 9001, which covers all parts of quality management, but it’s a specific system for welding quality. It includes rules for people, how welding is done, the tools used, checking the work, and keeping records. The standards are divided into different parts:
ISO 3834-1 – Choosing the right quality level: helps pick between Comprehensive, Standard, or Elementary based on how risky the product is.
(The new version, ISO 3834-1:2021, has replaced the older one from 2005.)
ISO 3834-2 – Comprehensive quality: the highest level, used for very important welds like pressure vessels and steel structures. It requires detailed planning, checking, and record-keeping.
ISO 3834-3 – Standard quality: for welds that aren’t too complicated, with a good but not extreme level of control.
ISO 3834-4 – Elementary quality: basic rules for simple or low-risk welding jobs.
ISO 3834-5 – List of important standards: includes other standards like ISO 9606, 14731, 15614, and 9712 that help follow these rules.
| Part | Title | Scope/Key Focus | Citation |
|---|---|---|---|
| ISO 3834-1 | Criteria for selecting level | How to choose between Parts 2 3 4 (based on product type and risk). | |
| ISO 3834-2 | Comprehensive quality requirements | Highest level (for critical/high-responsibility welding); demands thorough QA and records. | |
| ISO 3834-3 | Standard quality requirements | Mid-level (for medium complexity welds); adequate controls. | |
| ISO 3834-4 | Elementary quality requirements | Basic level (for simple or low-risk welds). | |
| ISO 3834-5 | Documents for conformity | References relevant welding standards (ISO 9606 etc.) required to implement Parts 2–4. |
ISO 3834 applies to both welding done in a workshop and on-site.It is required in some cases, like when structural steel is CE-marked under EN 1090 or when welding pressure equipment under the European PED. In many industries such as energy, automotive, rail, and oil & gas, it is not legally required, but customers often ask for it as proof that the welded products meet quality standards. Following ISO 3834 means setting up proper controls, like using approved welding procedures and records, ensuring welders are trained, keeping track of materials, and having plans for inspections. In practice, ISO 3834 is usually part of or connected to a company’s ISO 9001 quality management system, and it adds specific rules for handling welding as a special process.
Certification Lifecycle & Renewal Timeline
Certification to ISO 3834 goes through a series of audits. Usually, the process starts with an initial audit, which includes checking documents (Stage 1) and then visiting the workplace to check what is actually happening (Stage 2). After that, there are yearly checks to make sure everything is still working well. At the end of the three-year period, there is a full check to renew the certification.
For example, Pacific Certifications says the certificate is valid for three years with yearly checks.
SQS, a Swiss certification body, explains that the certificate lasts three years, with an annual audit and a final audit after three years.Some other organizations, like LRQA, offer a five-year certificate with yearly checks.
In practice, the steps are:
Stage 1 Audit (Documentation Review) – The certifier looks at the welding quality manual, procedure documents like WPS and PQR, qualifications, and compliance plans to check if everything is set up properly.
Stage 2 Audit (On-site Assessment) – The auditor visits the workplace to check how welding is being done, ensures procedures are followed, examines weld samples, looks at records such as NDT results, material information, and equipment calibration, and talks to staff.
Surveillance Audits (Years 1–2) – These are smaller audits, usually once a year, lasting about a day.
The auditor checks if the system is still working and makes sure any changes are properly documented.Pacificcert says these yearly audits help confirm that everything is still meeting the standards and catch any new changes in welding operations.
Recertification Audit (Year 3) – At the end of the three-year period, the whole process is reviewed again, similar to the initial audit.
If any issues are found, they need to be fixed.Once everything is in order, a new ISO 3834 certificate is issued for the next three-year cycle.
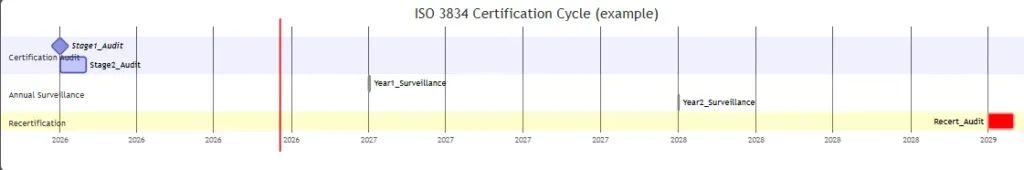
Illustration: A Gantt chart showing a standard ISO 3834 cycle in month/year format.
The first two stages of the audit happen at the beginning (for example, January 2026). Then, there are shorter surveillance audits during the first and second years (January 2027 and January 2028). The recertification audit takes place in the third year (January 2029).This cycle then starts again. (The exact dates and length of each phase may differ depending on the company’s preparedness and the auditor’s schedule.)
| Audit Type | Purpose | Approx. Timing | Notes |
|---|---|---|---|
| Initial Stage 1 | Review docs (WPS, qualifications, plans) | Before Stage 2 (could be combined) | Checks completeness, readiness. |
| Initial Stage 2 | On-site evaluation of implementation | Months 0–2 (after Stage 1) | Tests system on the shop floor. |
| Surveillance (Year 1) | Verify maintenance of system | ~12 months after certification | Annual check (often ~1 day) |
| Surveillance (Year 2) | Verify continued compliance | ~24 months after certification | Annual check (often ~1 day) |
| Recertification (Year 3) | Full re-audit for renewal | ~33–36 months after certification start | Similar scope to Stage 2; certificate renewed. |
Typical timelines: Getting ready to receive the final certificate usually takes 1–3 months if all the required documents are ready, as Pacificcert estimates 4–10 weeks depending on how well prepared everything is. Companies that have more processes, subcontractors, or multiple sites might need more days for audits, which means longer overall timelines.
Key point: ISO 3834 requires an annual check-up and a re-certification audit at the end of the certification period.
It’s important to plan a review before the certificate expires, usually 6–12 months in advance, to make any necessary improvements or schedule audits on time.
Triggers for Reassessment
Even though the fixed cycle helps with regular updates, there are certain events that should lead to a special review of the ISO 3834 system.Let your certifier know if:
– Scope Changes: Adding new products or welding methods, like using different materials, thicknesses, or types of joints, can make the current certificate not complete.
For example, if you go from making structural steel to building pressure vessels, you might need to upgrade from ISO 3834-3 to 3834-2 certification.
– Facility/Organizational Changes: Starting a new plant or moving welding work to a subcontractor, or combining two fabrication sites after a merger, means the quality management system needs to be checked again.
– Personnel Changes: If you lose your qualified Welding Coordinator (IWE, IWT, or IWS) or key people who write non-destructive testing (NDT) procedures or welding procedure specifications (WPS), it’s important to reassess.
These roles are required, and any changes need to be properly documented as ISO 3834 requires.
– Process Changes: Introducing automated systems, like robotic welding, new NDT techniques, or digital tools for tracking welds, should be reported.
These changes affect how processes are validated and recorded.
– Major Nonconformities: If an important audit finding happens, such as not showing proper procedure control or making unsafe welds, the certifier may ask for immediate action or a new audit.
– Regulatory or Standards Updates: If important rules or standards change, like a new edition of EN 1090, PED updates, or a revision of ISO 3834 parts, you must update your system. The certifier may need to check if you follow the new requirements.
– Customer/Supply-Chain Demands: Big customers or industry groups might require ISO 3834 certification (or a higher level than you currently have). This can force your company to reassess or expand your certification.
– Certificate Near Expiry: Start the renewal process about six months before your certificate expires.
This gives enough time for internal checks and planning audits, without letting the certificate expire.
In short, any major change that affects your welding quality system should be a reason to reassess. Certification bodies usually expect you to notify them of any scope changes so they can decide if they need to review or expand their audit.Not keeping up with these changes can lead to audit issues or parts of your certificate being invalid.
Renewal Process Step-by-Step
The ISO 3834 renewal process is similar to renewing other management systems, but with specific welding-related steps.Here’s a suggested order to follow:
- Management Review & Planning (Initial) – Set up a meeting between top management and important welding team members 6 to 12 months before the current certificate expires.
During this meeting, look at internal audit results, customer comments, process updates, and the current welding activities. Use this time to find any missing parts and set up the resources needed for renewal. - Internal Audit – Do a complete check of your welding quality system.
Use a checklist based on ISO 3834 to check if everything is up to standard.For example, make sure each welding procedure specification (WPS) has an active welding procedure qualification record (WPQR), that welders’ certificates match the jobs they are doing, and that material certificates are kept. Note any issues or areas that need improvement, and update procedures, records, or training as needed. - Pre-Assessment (Optional) – Some companies do a practice run or bring in an external expert to act like an auditor.
This helps find hidden issues, like missing records or unnoticed process problems. LRQA suggests doing a self-audit with an ISO 3834 checklist to help prepare. This step is not required but can make the real audit smoother. - Document Updates – Revise your welding procedures, control plans, or Welding Quality Manual to show changes since the last certification.
Make sure all documents, like welder qualifications, equipment calibration records, and NDT certificates, are current and organized. Have all required documents ready before the first audit stage to save time. - Stage 1 Audit (Documentation Review) – The certification body reviews your updated quality management system documents, procedures, and records.
They check that all necessary parts are in place. LRQA explains that Stage 1 mainly checks your welding quality management system documentation and confirms you are ready for the audit. Fix any small issues before moving to the next stage. - Stage 2 Audit (On-site Evaluation) – Auditors visit your workplace.
They talk to welders and inspectors, check how WPSs are being used, watch welding in progress, and look at completed welds and their records. They verify that the system is working as it should. LRQA describes Stage 2 as checking how well your welding quality management system is applied and if it’s effective, including looking at some contracts and production activities. Common problems found here might include missing records or not following the correct procedures (see next section). - Corrective Actions – The auditor will provide any nonconformity reports (NCRs).
Your team needs to handle each of these by finding the cause and then putting in written fixes. Often, these reports ask for new or updated procedures (like for repairs or tracking items) and retraining staff. Fix these reports quickly and keep track of progress. - Certification Decision – Once all major NCRs are resolved to the auditor’s satisfaction, the certification body will renew your certificate.
This usually happens within a few weeks after the audit if everything goes smoothly. The new certificate date will start the next cycle, which is often another 3 years. - Post-Audit Follow-up – Use any “opportunities for improvement” that the auditor points out to improve your quality management system.
Keep up with the annual check-ups and update your audit plan and management review plan with the lessons learned so your system keeps getting better until the next renewal.
Expert Tip: Keep a schedule for the certification process and assign someone to track each step.
Use an audit checklist (see below) to turn the renewal process into something you can manage step by step
Common Audit Findings & Mitigation Strategies
In our research and industry reports, commonly found issues (called nonconformities or NCRs) during ISO 3834/EN 1090 welding audits include:
- Welder Continuity Gaps: Welders must have valid certificates and be active every six months (as per ISO 9606-1/ASME IX).
Auditors often find missing records or expired certificates. To fix this, keep a signed log (physical or digital) showing each welder has done at least one weld in the past six months using the right method. Some welding machines can automatically record welding time by welder ID, which makes this easier. - WPS Accessibility Failures: The approved welding plans (WPS) must be available where the welding is happening.
Auditors often find that WPSs are stored in the office or versions are not properly managed. To fix this, keep printed or digital copies of WPSs on the shop floor, like on tables or tablets. Mark them clearly with the revision date. You can also use digital tools to send the correct welding settings directly to the machine. - Material Traceability Issues: It’s common to not properly link materials or parts to the final weld.
For instance, a filler wire lot might not be linked to a specific job, or base metal certificates could be missing. To fix this, label all materials (base metal and consumables) with unique IDs. Every filler wire spool, electrode box, and parent plate should have a certificate number. Use a traceability form or barcode system.Software dashboards can connect a weld’s details (like voltage and heat input) with batch numbers quickly. - Undocumented Repairs/Nonconformances: Sometimes weld repairs are done without proper records.
Auditors expect documented repair instructions and inspection reports. To fix this, set up a repair control process: decide when a weld needs repair, who approves it, and how it will be checked again (like with NDT). Keep detailed records of each repair and approval. Make sure your quality plan includes a “repair check” and that workers know to fill out NCR forms when needed. - Incomplete Welding Records: Auditors check production files and often find missing parts like incomplete PQRs or missing NDT reports.
They expect everything to be connected to a qualified process and person. To fix this, use a complete weld-pack system. When a job or batch is done, gather all the necessary documents: WPS and WPQR, welder certificates, base metal certificates (EN 10204), consumable logs, inspection reports, and acceptance records. PZVAR’s checklist looks for a complete sample production file. Fixing gaps now avoids auditor comments later. - Ineffective Internal Audit/CAPA: Not doing regular internal audits or taking too long to fix problems is often pointed out.
ISO 3834 auditors check if you are doing your own audits and fixing NCRs. To fix this, schedule internal audits specifically for welding (at least once a year). Track all audit findings until they are closed. Show through management reviews that issues are being handled properly.
In short, planning and good records are key to avoiding most problems.
Keeping updated logs, having easy access to procedures, and building a culture of recording issues helps the external audit go smoothly. Consider using digital welding management tools (for tracking welder activity, distributing WPSs, and managing weld records) – these tools not only help with compliance but can also turn audit data into real-time reports, as noted by industry experts.
Cost & Time Estimates; Resource Checklist
Estimating the resources needed to renew ISO 3834 depends on how big your operation is, how much work you do, and how mature your systems are. Important things to consider include how many welders you have, the welding methods you use, how many sites you operate from, and how complex your products are. In general:
- Timeframe: When you start preparing internally, Pacificcert says the typical certification cycle takes between 4 to 10 weeks.
This is assuming your documents are ready and you have a small-to-medium operation. If you already have procedures in place and your welders are qualified, the process is faster. For larger companies with many sites, over 50 welders, and complex Procedure Qualification Records (PQRs), the process takes longer. You’ll need more audit days and more documentation. Make sure to plan at least 6 months before your certificate expires, including time for internal audits and fixing any issues. - Certification Fees: The cost of an external audit can vary a lot depending on where you are and the certifier.
Auditors usually charge hundreds to a few thousand dollars per day. A 2- to 4-day certification audit (Stage 1 and 2) plus two 1-day surveillance visits might cost between $5,000 and $15,000 USD. Costs go up if you have many different welding methods, multiple locations, or if you’re being audited against multiple standards like ISO 9001. If you combine ISO 3834 with an existing management system audit, you might save some money. Pacificcert mentions that “certification costs depend on the number of welding operations, product complexity, testing and inspection needs.” - Internal Resources: You should assign someone to lead the project, often the Quality or Welding Coordinator.
Their tasks include doing the internal audit, updating your documents, tracking Corrective and Preventive Actions (CAPAs), working with the certification body, and gathering records. Involve department leaders like production, quality assurance, and purchasing early on. Give welders and inspectors time to collect logs and certificates. Management should also set aside a budget for internal preparation (like training or system upgrades) and for external audit fees.
Resource Checklist: Before the audit starts, make sure these are all in place:
- Welding QMS Documentation: A Welding Quality Manual or procedure that explains your ISO 3834 system (including scope, roles, and how things work).
Up-to-date Welding Procedure Specifications (WPS) and the Procedure Qualification Records (WPQR/PQR) that support them. Plans for inspection and testing. A document that names and qualifies the Responsible Welding Coordinator. - Personnel Qualifications: Valid certificates for all welders and welding operators (like ISO 9606 or ASME IX or a national equivalent) and Non-Destructive Testing (NDT) personnel (like ISO 9712).
Records showing welders have worked for at least six months. Proof that the appointed Welding Coordinator has an IWE/IWT/IWS or equivalent qualification. Proof of any needed training updates. - Equipment & Material Records: Logs showing how welding machines and measuring tools are calibrated and maintained.
Material test certificates (EN 10204 3.1/3.2) for base metals.Certified test reports for consumables like filler metals and electrodes, along with traceability labels. Records about environmental controls (like dry cabinets) for moisture-sensitive materials, if used. - Inspection and Test Records: Completed non-destructive testing reports (like VT/MT/PT/UT/RT) with criteria for what’s acceptable.
Records of dimensional checks if they are part of the audit scope. All in-process and final inspection reports logged. - Traceability Documentation: Job records connecting each weld to the welder, WPS, consumable batch, base material certificate, and inspection results.
For instance, a traveler or digital log for each weldment. - Nonconformance / Repair Records: Reports for any faulty welds, showing what went wrong and the steps taken to fix it.
Records of weld repairs, rechecks, and approvals. - Internal Audit and CAPA Records: Schedules and reports from internal audits, plus minutes from management reviews covering the welding process.
Logs of corrective actions taken in previous audits to close past nonconformances. - Management Review Outputs: Action plans or decisions made in recent management reviews related to welding.
Evidence that management has addressed resource needs and that the Quality Management System is still suitable for your goals. - Prior Audit Findings Closure: Make sure any issues found in the previous ISO 3834 audit have been completely resolved.
Auditors will check that past nonconformances were clearly dealt with and that they don’t happen again.
Pacificcert says that preparation involves “managing documentation, qualifying personnel, and checking that processes work.” Having this checklist ready can help speed up the audit and increase your chances of a smooth renewal.
KPIs and Monitoring Cadence
To keep the ISO 3834 system running smoothly between audits, it’s important to set up and keep track of specific welding-related KPIs. These metrics should match the quality and process goals and should be checked regularly, at least every three months, and during management reviews.Here are some examples:
- Weld Quality Metrics: Look at how many welds pass the first inspection (like VT or UT) compared to those that need fixes.
Also check how many welding defects or reworks happen each month. The goal is to keep the first-pass yield above 98%. - Welder and Procedure Metrics: Count how many welders are currently qualified versus those whose qualifications are about to expire.
Track how many welders are up-to-date with their training every six months. Also check how many active WPS/PQRs are in use compared to what is needed. The goal is to have 100% welder continuity, with all welders trained for their assigned tasks. - Inspection and NDT Results: Look at how often NDT (like MT or UT) inspections result in rejections.
Keep track of any major issues found in test results. The goal is to have zero critical rejections and quickly fix any minor ones. - Process and Equipment: Check how often equipment is down or not calibrated on time (like the percentage of machines calibrated as scheduled).
If you measure welding voltage and current, track how well the process parameters are followed. The goal is to have all important equipment calibrated and maintained on schedule. - Audit and CAPA: Track the number of internal audit findings and how they are changing over time.
Also look at how quickly non-conformities from audits or daily operations are fixed. Check how many scheduled internal audits are completed. The goal is to fix all findings within agreed time and complete 100% of the audit program. - Supply Chain: Keep a record of how many incoming material certificates are accepted versus returned.
Also track how many supplier welding system assessments are passed. The goal is to ensure all incoming materials can be traced back to their certificates, and key suppliers are certified as needed.
These KPIs should be shown in a simple dashboard or spreadsheet.
Review them during monthly or quarterly quality meetings. Top management should see overall trends during management reviews at least once a year to show ongoing improvement.If any KPI starts to go in the wrong direction, like if rework rates go up, take action quickly. Regularly checking these metrics not only helps improve the process but also gives strong proof to external auditors that the system is working effectively.
Case Studies & Hypothetical Scenarios
Case Study – Bridge Fabricator Expands Scope: A steel bridge maker had ISO 3834-3 certification for regular structural welding. When they started getting contracts for highway bridges that required thicker steel and more strict welding (like pedestrian bridges), they realized they needed ISO 3834-2. Six months before their current certification ended, the company checked their processes. Their quality team did an internal check, found they needed more WPQR tests for heavy steel plates, and updated their Welding Quality Manual. They did a pre-assessment audit on their own and fixed small issues. During recertification, the auditor saw everything was ready: new PQR tests were recorded, welders were retrained for the thicker plates, and the certificate scope was changed to match the higher standards. The renewal went smoothly.Lesson: Make sure your certification level matches your product needs and start preparing early if your scope changes.
Scenario – Merger of Fabrication Plants: Company A had ISO 3834-2 certification, and Company B had ISO 3834-3.
When they merged, they needed one single certification. They told their certifier and decided to move the less detailed scope up to Comprehensive (ISO 3834-2) to cover everything. They did joint internal checks at both sites, put together their documents into one Welding QMS instead of two, and trained staff under the new system. The external auditor then checked both locations in one visit.In the end, the merged company got a single ISO 3834-2 certificate that covered both plants.Lesson: Mergers and acquisitions need system integration and possible changes to the certificate scope; working with the certifier early is key.
Hypothetical – Regulatory Update Trigger: Imagine a new version of “EN 1090-1:2026” requires stricter welding oversight for steel structures, including new audit rules.
A fabrication shop that had ISO 3834-4 (elementary) and CE-marked products learned about this new rule.As a trigger, they decided to check their system. Their management review led them to switch to ISO 3834-3 to meet the new code. Over several months, they improved welder training and added a welding coordinator (IWS). They kept records of these changes and told their certifier. During the next audit, the auditors focused on the new requirements, like better traceability. The shop showed they met both the new EN 1090:2026 standard and the higher ISO 3834 level.Lesson: Keep an eye on changes in standards and regulations; updating your system early helps avoid being unprepared during audits.