EN 15085-2:2026
TBM
REQUIREMENTS
31 Aug 2026
EN 15085-2 2026 for Tunnel Boring Machines Complete Guide for Indian TBM Exporters
By Editorial Team
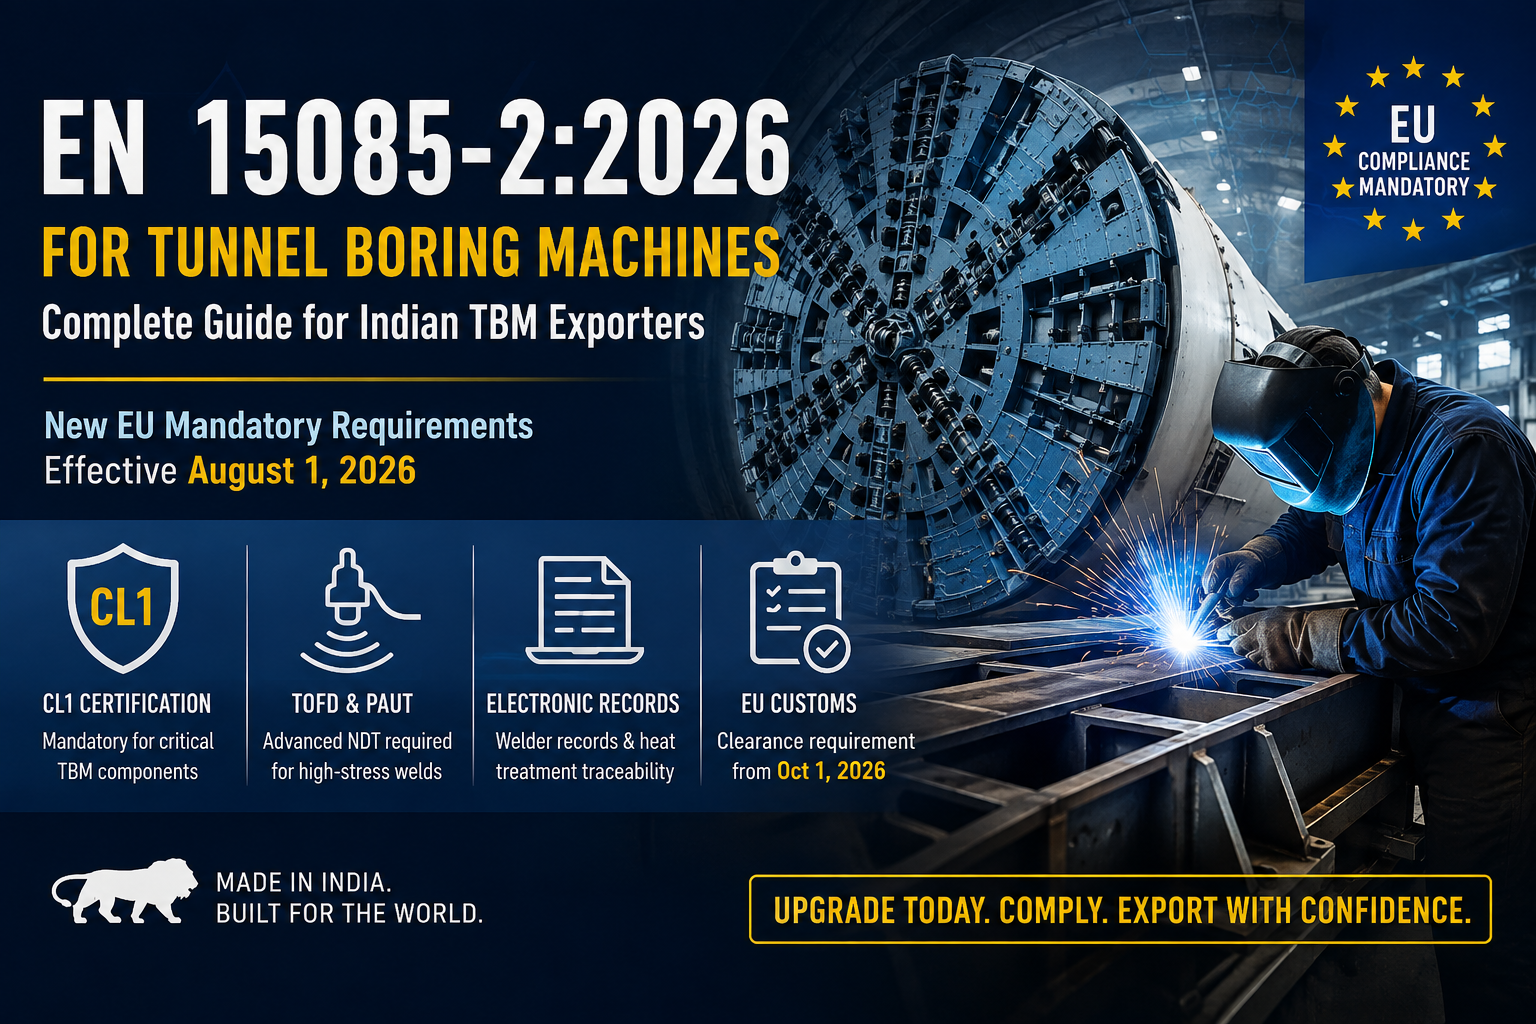
On August 1, 2026, the Official Journal of the European Union announced that EN 15085-2:2026 will become mandatory for steel welded parts made for full-face tunnel boring machines (TBMs) that are exported to the EU.
This update changes welding qualifications from being just a technical choice to a requirement for entering the market.
Now, CL1 certification is needed for certain safety-critical parts of TBMs.The article says that shipments without proper certification or with wrong certification will face customs delays starting from October 1, 2026.
For Indian manufacturers, exporters, and those who buy these products, following the rules is more than just getting a certificate.
They must also ensure their welding processes, non-destructive testing, welder qualifications, heat treatment, electronic records, traceability, and all customs paperwork are correct and in line with the new standards.
Upcoming Events
JLY
25
Welding Quality Webinar
Online
AUG
8
EN 15085 Transition Seminar
Berlin
SEP
14
India Certification Summit
Gurugram
See Also.....
Certification Alerts
- EN ISO 3834-4 transition deadline: 31 Dec 2024
- NABCB accreditation renewal — Updated requirements
What Changed on August 1, 2026?
The new requirements focus on important parts of the TBM that are welded together, such as:
– Main beams for TBMs used in hard rock
– Frames that support the cutterhead
– Structures that help with pushing the TBM forward
– Frames used to install segments
– Parts of the backup system that hold things together
The article says that many of these parts were earlier approved under CL2 or CL3.
However, because they are key to safety and must handle heavy loads, they now need to meet CL1 standards as part of the 2026 update.
| Date | Milestone | |
|---|---|---|
| August 1 | 2026 | EN 15085-2:2026 mandatory effect begins |
| Aug. 1-Oct. 1 | 2026 | Transition period |
| October 1 | 2026 | Customs clearance denial begins for uncertified/incorrectly certified shipments |
| November 1 | 2026 | Full enforcement stated in the article |
The article points out that suppliers who don’t have the necessary CL1 certification might have trouble getting their goods cleared by customs starting from October 1.
Why CL1 Certification Is Now Mandatory
CL1 is the top certification level mentioned in the article and is linked to welding that requires the strictest safety standards.
The main girders of the TBM and the support frames for the cutterhead go through heavy forces, shaking, and strong stress, which means the quality and ability to track the welding work are especially important.
| Level | Typical Applications | Safety Criticality | Testing |
|---|---|---|---|
| CL1 | Main girders, cutterhead frames, thrust rings | Highest | Full NDT, TOFD/PAUT, 100% traceability |
| CL2 | Secondary structural members, back-up frames | High | UT/RT, batch traceability |
| CL3 | Non-load-bearing components | Medium | Visual inspection + spot NDT |
For Indian manufacturers, here’s what needs to be considered:
– The current CL2 certification might not be enough for sending TBM equipment to the EU after October 1st.
– Welding coordinators must have the proper RWC Level A certification if they’re working within the CL1 scope.
– The WPS/WPQR documents might need to be requalified based on the CL1 testing standards.
– Welder qualifications should include the exact thicknesses, welding positions, and methods actually used in the work.
New NDT Requirements: TOFD and PAUT
One of the big changes mentioned in the article is the greater use of advanced non-destructive testing (NDT) for welds in high-stress areas of a TBM.
What Are TOFD and PAUT?
TOFD stands for Time-of-Flight Diffraction.
It uses ultrasonic signals that spread out from the edges of flaws to find and measure defects like cracks and poor welds.It works well for thick parts of the TBM’s main beams.
PAUT stands for Phased Array Ultrasonic Testing.
It uses probes with multiple elements and directs ultrasonic beams electronically.This method covers a wide area, works well on complex shapes, and saves digital records of each test.
Why Are TOFD and PAUT Important?
The article lists four main benefits:
– Better detection of flat flaws, especially cracks and poor fusion.
– Accurate measurement of defects through the full thickness of the weld, which helps determine how serious a problem is.
– Keeping digital records of scans that can be saved, reviewed, and studied again.
– Less exposure to radiation, since these methods do not need radiation safety areas, unlike other types of testing.
| TBM Component | Required NDT | Acceptance Criteria |
|---|---|---|
| Main girder butt welds | TOFD + PAUT | EN ISO 17640 Level 2 |
| Cutterhead support frame welds | PAUT | EN ISO 17640 Level 2 |
| Thrust ring circumferential welds | TOFD + PAUT | EN ISO 17640 Level 2 |
| Segment erector frame welds | PAUT or conventional UT | EN ISO 17640 Level 1 |
| Back-up system structural welds | Conventional UT or RT | EN ISO 17636 Level 2 |
The article also mentions that people who perform TOFD/PAUT tests need to have ISO 9712 Level 2 certification, proper training for the specific methods they use, and a good understanding of the weld shapes used in TBM.
Heat Treatment and Welder Traceability
EN 15085-2:2026 makes the rules for keeping electronic records about heat treatment and tracking welders stronger.
For parts that need post-weld heat treatment (PWHT), the standard says:
– Each part must have an electronic heat-treatment chart
– Temperature-time data must be recorded digitally
– It must include timestamps and where the temperature sensors were placed
– The furnace used must have a certificate of calibration connected to each batch
– The people doing the heat treatment must be qualified and have electronic records
– Electronic records for welders are now required instead of paper logs
These electronic welder records must include:
– Digital copies of welder qualifications
– Logs showing which welder did each specific weld
– Details of the welding parameters used, especially for automated or robotic welding
– A history of the welder’s performance, including any defects, rework, and results from non-destructive testing (NDT)
This ensures a clear link from the welder to the weld, then to the component, followed by NDT testing and finally certification.
Customs Clearance: What Happens at the Border?
The article explains that customs verification is an important step that comes from the new rules.
Customs Verification Process
1. Before goods arrive, customs checks the documents like the Declaration of Conformity, CL1 certificate, and NDT reports.
2. They also check if the certificate is still valid and covers the right things.
3. They look at the history of each part to make sure it matches records, welder logs, heat-treatment charts, and NDT reports.
4. If the papers are not complete or seem suspicious, customs might do a physical check or re-inspect using NDT methods.
Common Reasons for Rejection
The article lists the following issues that can lead to problems:
– Using CL2 or CL3 instead of CL1
– Missing TOFD or -PAUT reports
– Heat-treatment records that don’t match the part’s serial number
– Welder qualifications that have expired or are not suitable
– Certificates from the 2013 version instead of the 2026 version
Real-World Example
The article talks about a customs case in Rotterdam involving a shipment worth €3.2 million that was a TBM.There were some issues like a missing CL2 certificate, no TOFD reports, and paper records for heat treatment.
Extra costs were mentioned, such as getting emergency certification, redoing the NDT inspection, rebuilding digital records, paying demurrage fees, and facing contract penalties.
These added up to a total cost of €555,000.
Step-by-Step Compliance Roadmap
Indian manufacturers can follow this plan to get ready for CL1 certification.
1 Check your current certificate and make sure you know:
– What level of certification you have
– Which edition you’re using
– What parts are covered by the certification
– What TBM parts are included
2 List all the parts that are part of the certification, including:
– Main girders
– Cutterhead frames
– Thrust rings
– Other high-stress welded parts
3 Do an internal check to see where you stand.
Look at your WPS, WPQR, welder qualifications, NDT methods, heat treatment, and traceability to match the 2026 standards.
4 Hire a certification body.
Plan for Stage 1 and Stage 2 audits and think about how much time you might need.
5 Update your WPS and WPQR.
If needed, requalify your welding processes, including required tests like impact and macro checks.
Make sure welder qualifications include the real thickness of materials, welding positions, and processes used.
6 Use digital records for:
– Welder information
– Weld maps
– NDT reports
– Heat treatment logs
– Material tracking
7 Train your NDT staff in TOFD and PAUT or use qualified outside NDT experts.
8 Do a production test.
Make a sample part using updated methods and create full digital documents.
9 Finish the audits and get certified.
The timeline mentioned in the article is about:
| Period | Activity |
|---|---|
| Weeks 1–2 | Gap analysis and planning |
| Weeks 3–4 | Documentation upgrade |
| Weeks 5–6 | Production trial and internal audit |
| Weeks 7–8 | Notified Body audit and certification |
| Weeks 9–10 | Pre-shipment preparation |
Required Documentation Checklist
A compliant TBM export documentation package should include:
Certification
– EN 15085-2:2026 CL1 Certificate
– Information about the scope of the certificate
– Proof that the certificate is still valid
Welding Documentation
– Welding Procedure Specification (WPS)
– Welding Procedure Qualification Record (WPQR)
– Certificates showing welders are qualified
– Certificate showing the welding coordinator is qualified
– Weld maps
– Records of which welder worked on which weld
Non-Destructive Testing (NDT) Documentation
– TOFD reports
– PAUT reports
– Certificates showing NDT personnel are qualified
– Approved NDT procedures
– Records showing testing equipment is properly calibrated
Heat Treatment
– Electronic heat-treatment records
– Certificates showing the furnace is calibrated
– Qualifications of the person operating the heat treatment
– Heat treatment procedures
Traceability
– Material certificates
– Records showing where materials came from
– Identification numbers for each component
– Records linking welders to the welds they performed
Quality and Customs
– Factory Production Control (FPC) Manual
– Records of non-conformities and corrective actions
– Internal audit reports
– Management review records
– Declaration of Conformity
– Commercial invoice
– Packing list
– Certificate of Origin
– Bill of Lading
Digital files should also have clear and consistent names so that auditors and customs officials can easily find the required documents.
Common Mistakes and How to Avoid Them
Mistake 1: Thinking CL2 Is Enough
Problem: Current CL2 certificates are being used for TBM shipments going to the EU.
Fix: Move to the necessary CL1 certification and check what the certification covers.
Mistake 2: Using Regular UT Instead of TOFD/PAUT
Problem: Important welds in the main girder and cutterhead are being checked with just regular UT.
Fix: Use TOFD or PAUT methods, or work with approved service providers.
Mistake 3: Using Paper for Heat-Treatment Records
Problem: Paper charts are hard to check and verify.
Fix: Keep electronic records with timestamps for heat treatment.
Mistake 4: Welders Not Qualified for the Work They’re Doing
A welder who is qualified for thinner materials cannot be assumed to be qualified for thicker TBM parts.
Fix: Keep a qualification list that covers the real thickness, position, and welding method used.
Mistake 5: Missing Digital NDT Files
Just having a summary PDF might not include the full data needed for checks.
Fix: Keep the actual TOFD or PAUT files along with setup and calibration records.
Mistake 6: Using an Outdated Certificate
Problem: The certificate is based on EN 15085-2:2013 instead of the latest version from 2026.
Fix: Ask for an updated or new certificate under EN 15085-2:2026 when needed.
PZVAR Checklist vs EN 15085-2:2026
The article’s checklist maps practical audit preparation against the cited standard clauses:
| Topic | PZVAR Audit Guidance |
|---|---|
| Certification | Confirm CL1 certification |
| NDT | Use TOFD/PAUT for specified high-stress welds |
| Heat Treatment | Maintain electronic charts |
| Welder Traceability | Link welds to individual welders |
| WPS/WPQR | Requalify procedures where required |
| Welding Coordinator | Assign appropriate RWC Level A coordinator |
| NDT Personnel | ISO 9712 Level 2 + relevant TOFD/PAUT training |
| Material Traceability | Track materials through finished components |
| Electronic Records | Maintain digital records |
| Customs Documentation | Prepare CL1, NDT and heat-treatment documentation |
The original article presents this as a practical audit-preparation checklist alongside the cited EN 15085-2:2026 clauses.
Frequently Asked Questions
Q1. Can I ship TBM components with CL2 certification before October 1, 2026?
The article says this may be possible during the transition period but is not recommended, as buyers may already require CL1 and shipments arriving after October 1 could face rejection.
Q2. Do I need TOFD/PAUT for all TBM welds?
No. According to the article, TOFD/PAUT applies to specified critical welds such as main girder butt welds, cutterhead support frames, and thrust ring circumferential welds. Other structural welds may use conventional methods depending on requirements.
Q3. How long does CL1 certification take?
The typical timeline stated is 6–8 weeks, although some certification bodies may quote 8–10 weeks because of increased demand.
Q4. Can I use an external NDT provider?
Yes, provided the provider has the required ISO 9712 qualifications, TOFD/PAUT competence, and familiarity with TBM weld geometries and acceptance criteria.
Q5. What if my certificate is under EN 15085-2:2013?
The article states that such certificates do not cover the additional 2026 requirements and recommends upgrading to the 2026 edition.
Q6. Will customs check every TBM shipment?
The article describes customs verification as risk-based but states that CL1 documentation should be available for inspection from October 1, 2026.
Q7. What happens if a shipment is rejected?
Possible outcomes described include holding the shipment, emergency certification, NDT re-inspection, or re-export. Demurrage and other commercial costs can also arise.
Q8. Does EN 15085-2:2026 apply to non-EU TBM exports?
The article states that the mandatory requirement discussed applies to EU-bound shipments, while noting that similar requirements may be adopted elsewhere and that some EU-based project owners may specify CL1 for non-EU projects as well.
Conclusion
EN 15085-2:2026 sets a stricter standard for TBM welded parts, especially when it comes to CL1 certification, better non-destructive testing, welder skills, heat treatment records, and digital tracking.
For Indian TBM makers sending products to the EU, just having certification isn’t enough.
The whole welding process—from weld procedures and welder training to testing, heat treatment, material tracking, digital records, and paperwork—must all connect and be traceable.
The article mentions an October 2026 deadline for customs, so producers should start checking their current system and improving their certification well in advance.