EN ISO 3834 - 3
Requirements
Welding Quality
What Are the EN ISO 3834-3 Requirements for Welded Products? Welding Quality Certification in Pune
By First Welding Certification Technical Editorial Team
6 Min Read Time
13 Oct 2026
Table Of Contents
- Introduction
- What Is EN ISO 3834-3?
- What Are the Main EN ISO 3834-3 Requirements?
- Welding Quality Controls for Welded Products
- EN ISO 3834-3 Documentation and Quality Records
- Which Manufacturers Should Consider EN ISO 3834-3?
- How to Prepare for EN ISO 3834-3
- Frequently Asked Questions
- Related Searches
- Conclusion
EN ISO 3834 - Certification
EN ISO 3834 -1
EN ISO 3834 -2
EN ISO 3834 -3
EN ISO 3834 -4
Introduction
How can welding manufacturers maintain consistent product quality and meet customer requirements? The answer starts with proper welding controls, competent personnel, suitable equipment and effective production planning.
EN ISO 3834-3 standard quality requirements for fusion welding of metallic materials. It covers welding work done in workshops and at installation sites, enabling manufacturers to set up controls that match their specific welding processes.
For Indian manufacturers producing welded steel structures, industrial equipment, machinery and metal components, understanding EN ISO 3834-3 is important when assessing applicable welding quality requirements.
This blog explains EN ISO 3834-3 requirements, welding quality controls, relevant documentation, and how manufacturers can prepare for a conformity assessment.
What Is EN ISO 3834-3?
EN ISO 3834-3 is part of the EN ISO 3834 series, which defines quality requirements for fusion welding of metallic materials.
The standard establishes a framework for controlling welding operations so manufacturers can meet specified quality requirements. It includes relevant activities starting from reviewing technical requirements up to managing welding production and associated quality control measures.
The EN ISO 3834 series includes different quality requirement levels:
- EN ISO 3834-2: Comprehensive quality requirements.
- EN ISO 3834-3: Standard quality requirements.
- EN ISO 3834-4: Elementary quality requirements.
The appropriate level depends on the product, manufacturing conditions, contractual obligations and applicable product standards. Manufacturers should assess these factors before deciding which requirements apply.
What Are the Main EN ISO 3834-3 Requirements?
EN ISO 3834-3 addresses several areas that influence welding quality. Manufacturers should review the applicable clauses and establish controls suited to their products and production activities.
Review of Requirements and Technical Review
Before production starts, manufacturers should understand customer specifications, engineering drawings, material requirements and applicable acceptance criteria.
A technical review helps identify whether the organisation has the necessary personnel, equipment, procedures and production capabilities to complete the welding work.
Welding Personnel
Personnel involved in welding must have competence appropriate to their assigned activities.
Manufacturers must identify and establish the appropriate qualification criteria for welders, welding operators, and welding coordination personnel. Relevant records should be maintained according to the work scope and governing requirements.
Inspection and Testing Personnel
Inspection activities must be performed by personnel with the competence required for their assigned tasks.
Where non-destructive testing is required, manufacturers should establish the relevant personnel qualification arrangements and retain applicable records.
Equipment Suitability and Maintenance
Welding equipment must be suitable for the production activities being performed.
Manufacturers should maintain equipment in appropriate working condition and address the calibration or validation of measuring, inspection and test equipment where applicable.
Welding Procedures and Production Planning
Production planning should identify the welding activities, resources, instructions and controls needed to achieve the specified results.
Manufacturers should establish Welding Procedure Specifications and ensure the necessary procedure qualifications are available when required. Work instructions should communicate relevant production requirements to personnel.
Storage and Handling of Materials
Parent materials and welding consumables need appropriate storage and handling arrangements.
Manufacturers should prevent material mix-ups, deterioration and contamination that could affect the quality of welded products. Identification and traceability must comply with the relevant technical and contractual requirements..
Post-Weld Heat Treatment
Where post-weld heat treatment is required, manufacturers should establish suitable arrangements for performing and controlling the treatment.
The applicable requirements depend on the material, product specifications and relevant technical standards.
Welding Quality Controls for Welded Products
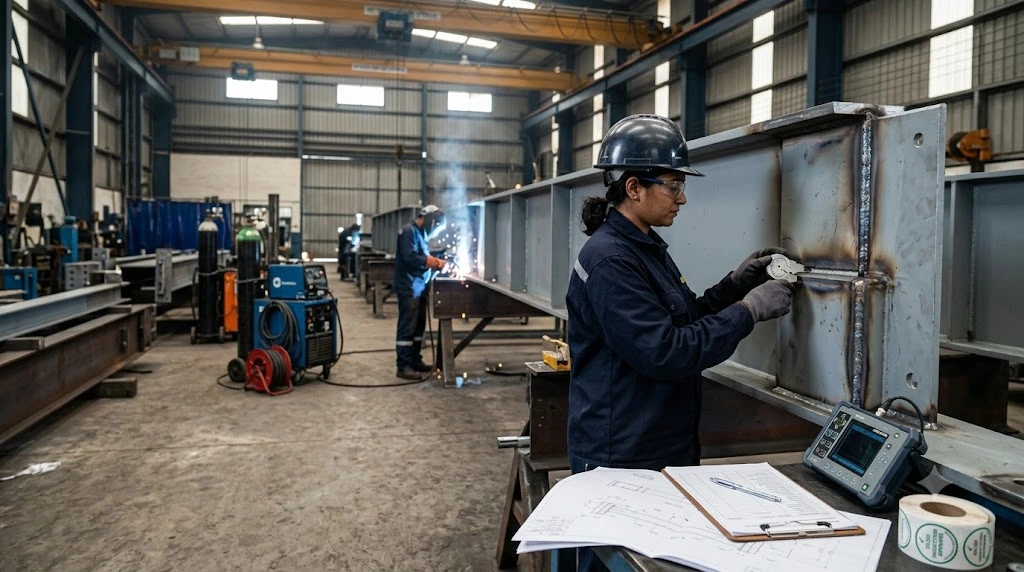
Applying EN ISO 3834-3 involves controlling welding activities throughout production rather than inspecting the finished product alone.
Before Welding
Manufacturers should review drawings, confirm material requirements, verify the availability of applicable welding procedures and check personnel competence.
Joint preparation, equipment readiness and consumable handling should also meet the specified requirements.
During Welding
Production personnel should follow the relevant welding procedures and work instructions.
Manufacturers should monitor the required production parameters and maintain applicable records. Any deviations should be assessed and addressed according to established controls.
After Welding
Completed welds should undergo the inspection and testing specified for the product.
Depending on the requirements, this may include visual examination, dimensional inspection or non-destructive testing. Acceptance criteria should come from the applicable drawings, specifications and standards.
When inspection identifies a defect, the manufacturer should control the non-conforming work and determine the appropriate action before acceptance.
EN ISO 3834-3 Documentation and Quality Records
Documentation helps manufacturers demonstrate that welding activities follow the specified requirements.
Depending on the applicable scope, relevant records may include:
Technical and contract review records.
Welding procedure specifications and applicable qualification documents.
Welder and welding operator qualification records.
Personnel competence and welding coordination records.
Material identification and traceability records, where required.
Equipment maintenance and applicable calibration records.
Inspection and test reports.
Post-weld heat treatment records, where applicable.
Records of non-conformities and corrective actions.
Manufacturers should maintain records in an organised, accessible manner. The exact documentation requirements must be verified against the applicable edition of the standard and the product specifications.
Which Manufacturers Should Consider EN ISO 3834-3?
EN ISO 3834-3 may be relevant to organisations carrying out fusion welding of metallic materials where standard quality requirements are appropriate.
Examples include:
Industrial machinery and equipment producers.
Welded metal component manufacturers.
General engineering and fabrication businesses.
Manufacturers producing welded assemblies for industrial applications.
Organisations working under specific product standards may face additional requirements. For example, structural steel manufacturers working under EN 1090 or railway welding manufacturers working under EN 15085 should evaluate the requirements applicable to their particular products and activities.
How to Prepare for EN ISO 3834-3
Manufacturers can use the following steps to review their readiness.
Step 1: Identify applicable requirements. Review customer contracts, product specifications, drawings and relevant standards.
Step 2: Assess welding personnel. Verify the competence and qualifications required for the assigned welding, coordination and inspection activities.
Step 3: Review procedures and equipment. Check welding procedures, equipment suitability, maintenance and applicable calibration arrangements.
Step 4: Examine material controls. Review material identification, storage, handling and traceability where required.
Step 5: Check inspection arrangements. Confirm that inspection methods, personnel and acceptance criteria meet applicable requirements.
Step 6: Review documentation. Identify missing records and establish a practical plan to address gaps.
Step 7: Confirm the assessment route. Determine the applicable conformity assessment or certification arrangements with the relevant customer, product standard or certification body.
These steps provide a starting point for a structured review, not a substitute for a formal clause-by-clause assessment.
Frequently Asked Questions
What is the difference between EN ISO 3834-2 and EN ISO 3834-3?
EN ISO 3834-2 covers comprehensive quality requirements, while EN ISO 3834-3 covers standard quality requirements. The applicable level depends on product and contractual requirements.
Is EN ISO 3834-3 suitable for every welding manufacturer?
No. Manufacturers should determine the appropriate quality requirement level based on the nature of their welding operations, product specifications and applicable standards.
What documents are relevant to EN ISO 3834-3?
Relevant records may include welding procedures, personnel qualification documents, equipment records, material identification records and inspection reports. Exact requirements depend on the applicable scope.
Does EN ISO 3834-3 automatically permit CE marking?
No. EN ISO 3834-3 alone does not automatically establish eligibility for CE marking. Applicable European legislation, product standards and conformity assessment requirements must also be considered.
Is EN ISO 3834-3 the same as ISO 9001?
No. ISO 9001 addresses quality management systems across an organisation, whereas EN ISO 3834-3 specifically addresses standard quality requirements for fusion welding of metallic materials.
Related Searches
Conclusion
EN ISO 3834-3 provides a structured framework for managing welding quality in manufacturing and field installation activities. Its requirements address technical review, personnel competence, equipment, production planning, material handling and other controls that influence the quality of welded products.
For Indian welding and fabrication manufacturers, understanding the applicable requirements can help identify gaps in production controls and documentation before a customer assessment or certification process.
The key is to select the appropriate quality requirement level and implement controls that match the actual products, welding activities and applicable standards.
Are your welding quality controls aligned with the requirements applicable to your products?
First Welding Certification Pvt Ltd (PRVÁ ZVÁRAČSKÁ, a.s.) — Explore EN ISO 3834 certification requirements and discuss the relevant conformity assessment process for your organisation.